

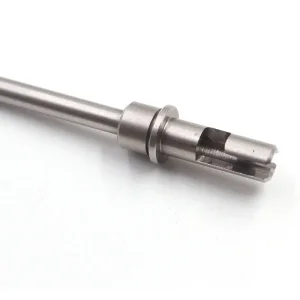

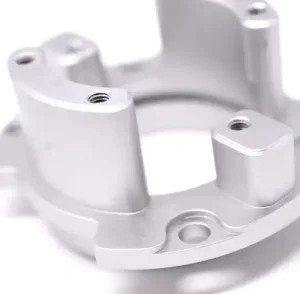
The global motorcycle component aftermarket and OEM assembly market is experiencing an unprecedented technical evolution. Valued at over $14.2 billion globally, the industry has shifted away from traditional sand casting and heavy cast-iron structures toward high-precision, billet-machined Custom CNC Motorcycle Parts. Today's powersports buyers—ranging from professional SBK/MotoGP racing syndicates to niche electric motorcycle OEMs and bespoke custom builders—demand componentry that achieves maximum structural rigidity while reducing unsprung weight to absolute mechanical limits.
SEO Information Gain Insight: Modern semantic search intent in powersports engineering centers on material density, dimensional repeatability, and surface fatigue resistance. Standard off-the-shelf components often fail to meet high-vibration requirements, forcing engineering teams to source custom 5-axis CNC machined parts with verified material test reports (MTR) and coordinate measuring machine (CMM) tolerance audits.
As a specialized custom CNC motorcycle parts supplier and precision service provider, Sunmy Hardware bridges the gap between digital CAD design and high-volume industrial production. Operating from Shenzhen’s advanced manufacturing ecosystem, we leverage multi-axis CNC milling, high-speed Swiss lathe turning, aluminum die casting, and progressive metal stamping to fulfill complex mechanical blueprints. Whether producing single-piece titanium prototype rearsets or thousands of hard-anodized billet triple clamps, our facility adheres to strict ISO 9001:2015 process controls.
Generative Design & FEA Topology
By leveraging Finite Element Analysis (FEA) combined with generative algorithms, modern motorcycle chassis parts eliminate non-critical mass. 5-axis CNC machining translates complex organic computer models into physical aluminum 7075-T6 parts that maintain structural integrity under extreme torsional loads.
Aerospace-Grade Alloy Shifts
The industry is transitioning from standard 6061 aluminum to AL 7075-T6 (Yield Strength: ~505 MPa) and Titanium Ti-6Al-4V (Grade 5). These materials provide exceptional strength-to-weight ratios for critical components like front wheel axles, swingarm pivots, and engine head bolts.
Advanced Tribological Coatings
Performance components require specialized surface treatments. Hard Anodizing Type III (MIL-A-8625), Physical Vapor Deposition (PVD), and Diamond-Like Carbon (DLC) coatings drastically cut friction coefficients on suspension stanchions, engine valve stems, and custom sprocket teeth.
1. Superbike & Track Racing
Key Parts: Adjustable rearsets, clip-on handlebars, quick-shifter linkages, custom radial brake calipers, magnesium/aluminum wheel hubs.
Requirement: Millimeter-accurate ergonomic adjustment, high impact resistance under track crashes, heat-sink fins for thermal regulation.
2. Bespoke Custom & Chopper Builds
Key Parts: Billet triple trees, custom rake clamps, forward controls, carved engine timing covers, decorative air cleaner housings.
Requirement: Show-quality mirror polishing, intricate 3D CNC surface engraving, custom anodized colors, flawless cosmetic aesthetics.
3. Electric Motorcycles (e-Powersports)
Key Parts: Liquid-cooled battery enclosures, electric motor mounting plates, planetary gear reduction housings, thermal interface plates.
Requirement: IP67 waterproof sealing faces, high thermal conductivity aluminum alloys, EMI/RFI shielding, vibration damping structures.
4. Off-Road, Enduro & Motocross
Key Parts: Heavy-duty skid plates, chain guides, reinforced suspension linkages, CNC footpegs with hardened stainless steel teeth.
Requirement: High fatigue resistance, debris protection, self-cleaning mud channels, corrosion-resistant anodizing.
| Material Alloy | Tensile Strength | Primary CNC Machining Applications | Recommended Surface Finish | Achievable Tolerances |
|---|---|---|---|---|
| Aluminum 6061-T6 | 310 MPa | Frame brackets, covers, foot pegs, license plate holders | Clear/Color Anodizing, Bead Blast | ±0.010 mm |
| Aluminum 7075-T6 | 572 MPa | Billet triple clamps, sprockets, rearsets, suspension arms | Hard Anodize Type III (50μm) | ±0.005 mm |
| Titanium Ti-6Al-4V (Gr5) | 950 MPa | Axles, brake rotor bolts, engine valves, exhaust flanges | PVD Coating, Anodized Titanium Colors | ±0.005 mm |
| Stainless Steel 316L / 17-4PH | 750–1100 MPa | High-pressure hydraulic fittings, brake pistons, fasteners | Electropolishing, Passivation | ±0.008 mm |
| Brass / Bronze Alloys | 400–650 MPa | Bushings, vintage trim caps, carburettor components | Raw Polished, Clear Coat | ±0.010 mm |
DFM Engineering & Cost Optimization
Our engineering team performs strict Design for Manufacturability (DFM) reviews on every incoming 3D STEP/IGES file. We identify tool path bottlenecks, undercut complications, and unnecessary tight tolerances—recommending modifications that reduce machining cycle times by up to 35% without altering physical function.
Full-Spectrum Quality Control (CMM & FAI)
Every custom order is backed by First Article Inspection (FAI) reports and full dimensional CMM scanning. We verify thread pitch tolerances, bore concentricity, and surface roughness before mass runs. Material mill test reports (MTR) guarantee material purity and compliance.
IP Protection & Direct Factory Supply
We enforce strict non-disclosure agreements (NDAs) to protect proprietary motorcycle designs and performance inventions. As a direct Shenzhen OEM manufacturer with integrated CNC machining, stamping, die casting, and assembly, buyers eliminate agent markups and receive transparent factory pricing.
What types of custom CNC motorcycle parts can Sunmy Hardware manufacture?
We manufacture a comprehensive array of motorcycle parts including billet aluminum triple clamps, adjustable rearsets, clip-on handlebars, engine timing covers, brake caliper adapters, wheel hubs, sprockets, frame sliders, suspension linkages, and custom electric motorcycle powertrain housings. We work from 2D/3D CAD drawings or physical samples for reverse engineering.
What aluminum grades are best suited for high-performance motorcycle components?
For structural and high-stress components such as triple clamps, rearsets, and rear sprockets, Aluminum 7075-T6 is strongly recommended due to its exceptional yield strength (~505 MPa) and fatigue resistance. For non-structural covers, reservoir caps, and visual trim, Aluminum 6061-T6 provides outstanding anodizing quality, excellent corrosion resistance, and cost efficiency.
What tolerances can Sunmy Hardware hold on critical CNC turned and milled motorcycle parts?
Our high-precision 5-axis CNC machining centers and Swiss CNC lathes achieve standard tolerances of ±0.010 mm. For critical bearing seats, shaft bores, and hydraulic valve housings, we reliably hold micro-tolerances down to ±0.005 mm. All dimensions are verified using optical comparators and CMM machinery in temperature-controlled environments.
Do you offer prototype machining as well as high-volume production runs?
Yes. We support single-piece rapid prototyping through 3-axis/5-axis CNC milling, 3D metal printing (SLM), and low-volume bridge runs. Once designs are validated, we scale effortlessly to high-volume production using dedicated multi-station CNC centers, automated aluminum die casting, and progressive sheet metal stamping tooling.
What surface treatments and anodizing finishes are available?
We provide full-spectrum surface finishing in-house and through audited partners. Options include Type II Decorative Color Anodizing (Black, Red, Gold, Blue, Titanium grey), Type III Hard Anodizing (MIL-A-8625 for extreme wear resistance), Bead Blasting (Glass bead, aluminum oxide), Mirror Polishing, Powder Coating, Electropolishing, and PVD/DLC friction coatings for racing components.
How do you handle intellectual property (IP) protection and NDA agreements?
We prioritize IP security. Before receiving 3D CAD files or proprietary product drawings, we sign binding Non-Disclosure Agreements (NDAs). Your design files remain encrypted on our secured internal servers and are never shared with third-party brokers or unauthorized entities.