
Featured Plastic Injection Molded Components
Explore our precision-engineered molded components manufactured for global OEM/ODM applications across automotive, medical, industrial, and consumer sectors.




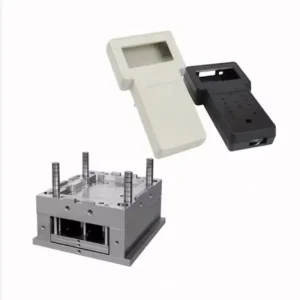



1. Global Commercial & Industrial Status of Plastic Injection Molding
The global plastic injection molding market size, valued at over USD 285 billion in recent industrial analyses, is projected to grow at a CAGR of 4.8% through 2030. This growth is driven by structural shifts across four core industrial verticals: automotive electrification, medical device miniaturization, smart industrial automation, and consumer electronics convergence.
Automotive & EV Shift
The structural transition toward Electric Vehicles (EVs) requires drastic weight reduction. Lightweight polymers (PA66, PBT, PEEK) replace traditional die-cast metal brackets, battery cell carriers, and high-voltage busbar connectors without sacrificing tensile strength or thermal rating.
Medical Device Rigor
Next-generation diagnostic tools, wearable monitoring housings, and surgical fluid systems demand cleanroom ISO 13485 production environments, bio-compatible polymers (LSR, medical PC), and micro-molding tooling capable of holding micron-level feature tolerances.
IoT & Electronics Enclosures
Edge-computing hardware, POS terminals, and industrial IP67 ruggedized sensors mandate multi-material overmolding (TPE over ABS/PC) for enhanced impact protection, IP-grade sealing, and ergonomic user interfaces.
Information Gain Insight: Modern polymer selection is no longer just about choosing between commodity resins (PP, PE) vs. engineering resins (ABS, PC). Global procurement leadership requires analyzing polymer rheology, gate shear rates, crystalline vs. amorphous shrink rates, and anisotropic fiber orientations during the initial DFM phase to guarantee dimensional stability post-mold.
Sunmy Hardware Operational Excellence Metrics
Data-driven tooling engineering, tight process controls, and verified international delivery performance.
In-House Mold Making & Engineering
Equipped with high-speed CNC machining centers, mirror EDM (Electrical Discharge Machining), and precision slow-wire cutting technology. Sunmy Hardware designs and fabricates Class 101 high-cavitation steel molds (S136, NAK80, H13) capable of exceeding 1,000,000 production cycles.
Integrated Secondary Operations
Beyond raw injection molding, our facility offers turnkey value-added solutions including ultrasonic welding, multi-color pad printing, silk screening, vacuum metallization, precision CNC post-machining, and cleanroom packaging.
2. The China Advantage: Precision Ecosystem & Supply Chain Speed
For international OEMs, sourcing custom plastic injection molded components from Shenzhen, China is no longer merely a cost-saving measure—it is a strategic speed-to-market necessity. The Greater Bay Area represents the world's most concentrated ecosystem for mold design, material formulation, and tool manufacturing.
| Evaluation Parameter | Western Domestic Tooling (US / EU) | Sunmy Hardware (Shenzhen Ecosystem) | Strategic Procurement Benefit |
|---|---|---|---|
| T1 Sample Lead Time | 8 to 14 Weeks | 14 to 21 Days | Accelerates product launch cycles by up to 75%. |
| Tooling Cost Structure | High Overhead ($25,000 - $80,000+) | Optimized ($5,000 - $22,000) | Drastically lowers NRE (Non-Recurring Engineering) capital expenditure. |
| Multi-Process Integration | Segmented (Separate moldmaker, molders, coaters) | Turnkey In-House (Tooling + Molding + Finishing) | Eliminates vendor handoff friction and liability ambiguity. |
| Engineering DFM Flexibility | Rigid change request protocols & fees | 24-Hour DFM Iteration & Moldflow® Support | Rapid optimization of draft angles, ribs, and gate placements. |
| Resin & Insert Sourcing | Long lead-times for specialty polymers | Direct OEM Resin & Brass/Steel Insert Network | Guarantees material authenticity (RoHS/REACH) with verified COAs. |
Unrivaled Cluster Density & Material Synergy
Located in Shenzhen's manufacturing hub, Sunmy Hardware leverages real-time access to regional specialty resin compounders, masterbatch engineers, custom hot runner system builders (Yudo, Mold-Masters, Synventive), and specialized surface texturing providers (Mold-Tech standards). This proximity ensures that complex engineering challenges—such as glass-fiber orientation warpage or flame-retardant blooming—are resolved in days rather than months.
3. Localized Industrial Application Scenarios
Precision plastic injection molding is highly application-specific. Mechanical requirements, chemical exposure, thermal range, and aesthetic targets dictate tooling architectures and resin specifications. Below is an engineering breakdown of Sunmy Hardware’s specialized application domains:
Automotive Powertrain & Sensor Housings
Resin Choice: PA66-GF30 (30% Glass Fiber Reinforced Polyamide) or PBT-GF20.
Engineering Challenge: High under-hood temperatures (150°C+), continuous vibrational fatigue, exposure to automotive fluids, and tight pitch tolerances for embedded copper terminals.
Sunmy Solution: Automated insert molding using vertical rotary injection machines. Precision core-pulling mechanisms maintain pin positioning within ±0.01mm, preventing flash around delicate brass/copper terminals.
Precision Optical Lenses & Transparent Covers
Resin Choice: High-Purity Optical Grade Polycarbonate (PC) or PMMA.
Engineering Challenge: Eliminating internal stresses, flow lines, black spots, and birefringence that compromise optical clarity.
Sunmy Solution: Class 100,000 cleanroom injection molding, electric injection units with ultra-precise injection speed profiling, mirror-polished S136 mold cavities (SPI A1 finish), and controlled variotherm mold temperature management.
Industrial Power Tools & Ergonomic Handles
Resin Choice: Two-Shot Overmolding (Substrate: Rigid ABS/PC Blend; Overmold: Soft TPE/TPU).
Engineering Challenge: Achieving permanent chemical bonding between rigid substrate and soft grip, preventing delamination under intense drop-impact and oil contact.
Sunmy Solution: Advanced 2K dual-shot injection molding with rotating platen molds. Precise mechanical interlocks engineered into substrate drawing, combined with optimized melt temperature overlap for superior chemical adhesion.
High-Precision Power Transmission Gears
Resin Choice: Unfilled or PTFE-lubricated Polyoxymethylene (POM / Acetal).
Engineering Challenge: Gear tooth profile accuracy (AGMA Class 8-10 targets), controlling volumetric shrinkage, avoiding void formation in thick gear hubs.
Sunmy Solution: Multi-gated balanced cold runner tooling, holding pressure curve optimization during crystallization phase, and 100% gear mesh concentricity inspection via optical shaft measuring machines.
4. Strategic Procurement Framework & E-E-A-T Quality Assurance
Navigating overseas supplier selection requires rigorous verification of technical competence, tooling maintenance protocols, and dimensional inspection systems. Below is Sunmy Hardware's engineering standard operating procedure (SOP) built around Google E-E-A-T principles (Experience, Expertise, Authoritativeness, and Trustworthiness).
Stage 1: DFM & Moldflow® Analysis
Before steel is cut, Sunmy engineers conduct comprehensive Design for Manufacturability (DFM) reviews. Utilizing Autodesk Moldflow® software, we analyze fill time, packing pressure distribution, weld line locations, air traps, and volumetric shrinkage. Wall thicknesses are audited for uniform transitions (recommended 1.5mm–3.0mm) to mitigate sink marks.
Stage 2: Tool Steel Qualification
Tool steel choice directly influences part surface finish, cycle times, and mold lifespan. We certify every block of tool steel with steel mill heat-treatment documentation. We offer HASCO, DME, and MISUMI standard components for seamless global maintenance.
Stage 3: Scientific Injection Molding
We implement decoupled (Scientific) injection molding processes (Stage I Fill, Stage II Pack/Hold, Stage III Cool). By decoupling fill speed from packing pressure, we establish repeatable, machine-independent process windows that protect against part weight variance across batch runs.
Tool Steel Selection Matrix for Procurement Buyers
| Tool Steel Grade | Hardness (HRC) | SPI Surface Finish Polish | Expected Mold Life (Cycles) | Recommended Resin Applications |
|---|---|---|---|---|
| P20 (1.2311) | 28 - 32 HRC | SPI B-2 (Medium Polish) | 300,000 | Commodity Resins (PP, PE, ABS), Prototype Tooling |
| NAK80 | 38 - 42 HRC | SPI A-2 (High Polish) | 500,000 | ABS, PC/ABS, High-Appearance Consumer Housings |
| S136 (Stainless) | 48 - 54 HRC | SPI A-1 (Super Mirror) | 1,000,000+ | Corrosive Resins (PVC), Medical Grade, Optical Lenses |
| H13 (1.2344) | 48 - 52 HRC | SPI B-1 (Fine Satin) | 1,000,000+ | Abrasive Glass-Filled Resins (PA66-GF30, PBT-GF) |
Quality Assurance & Traceability Guarantee: Every production batch at Sunmy Hardware is backed by raw material Certificate of Analysis (COA), RoHS/REACH compliance documentation, First Article Inspection (FAI) reports generated via ZEISS Coordinate Measuring Machines (CMM), and SPC (Statistical Process Control) data tracking critical Cpk dimensions.
5. Future Trends: Smart Molding & Sustainable Polymer Technology
As the injection molding sector adopts Industry 4.0 practices, Sunmy Hardware is at the forefront of integrating smart factory automation, real-time cavity pressure sensing, and eco-friendly polymer processing.
In-Cavity Pressure Sensors
By placing RJG® piezo-electric pressure sensors directly inside mold cavities, our injection units automatically adjust hold-pressure switches in real time based on actual resin viscosity changes, eliminating short shots and flash.
PCR & Bio-Polymer Processing
To support global sustainability goals, Sunmy Hardware has optimized mold gating and temperature control to process up to 100% Post-Consumer Recycled (PCR) resins (rPET, rPP, rABS) and PLA bio-plastics without degrading tensile integrity.
Micro-Molding & LSR Precision
Expanding capabilities into Liquid Silicone Rubber (LSR) and micro-molding allows us to manufacture medical seals, micro-valves, and optical gaskets weighing less than 0.1 grams with extreme tear strength and chemical inertness.
6. Frequently Asked Questions (Industrial Procurement FAQ)
Additional Specialized Molded & Precision Components
Discover our complete scope of multi-material injection molding, silicone molding, turned connectors, and automotive component solutions.



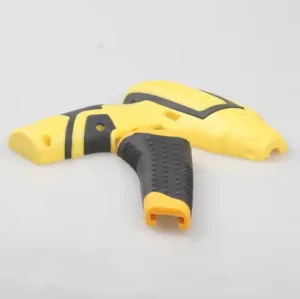


Ready to Accelerate Your Plastic Injection Tooling Project?
Partner with Shenzhen Sunmy Hardware Co., Ltd. for engineering-grade DFM feedback, rapid T1 tooling execution, and verified high-volume manufacturing export services.