Engineered Metal & Plastic OEM Components
Direct factory manufacturing with CMM dimensional reports and material certifications.



Understanding ODM Aluminum Injection Casting: Physics & Metallurgy
Aluminum Injection Casting—broadly encompasses High-Pressure Die Casting (HPDC), Vacuum-Assisted Die Casting, and Thixocasting/Semi-Solid Injection Molding—is the cornerstone of modern lightweight structural engineering. By injecting molten or semi-solid aluminum alloys into hardened tool steel molds at velocities exceeding 40 m/s and under extreme intensification pressures (ranging from 300 to 1,400 bar), manufacturers achieve near-net-shape components with complex geometric thin walls down to 1.0mm.
Intensified Injection Dynamics
Controlled shot sleeve filling prevents air entrapment. High hydraulic intensification guarantees void reduction and dense microstructures during the critical fraction-of-a-second solidification window.
DFM & Moldflow Simulation
Every drawing undergoes MAGMA/Flow-3D thermal and fill velocity modeling to eliminate thermal shock, hot tears, and shrinkage porosity before steel cutting commences.
Structural Grain Refinement
Rapid thermal dissipation against cooled tool walls creates an ultra-fine grain surface boundary layer, delivering high fatigue resistance and superior mechanical yield strength.
Comprehensive Aluminum Alloy Engineering Matrix
Choosing the precise aluminum alloy for high-pressure injection molding determines thermal conductivity, tensile strength, yield strength, fluid castability, and post-machining dimensional stability.
| Alloy Grade | Tensile Strength (MPa) | Yield Strength (MPa) | Thermal Cond. (W/m·K) | Elongation (%) | Primary Industrial Applications |
|---|---|---|---|---|---|
| A380 (ADC10) | 320 | 160 | 96.2 | 3.5% | General electronics enclosures, motor brackets, chassis components. Best overall fluid castability. |
| ADC12 (A383) | 310 | 150 | 96.0 | 3.5% | High-complexity intricate geometries, automotive engine covers, telecommunication housings. |
| A360 | 317 | 170 | 113.0 | 5.0% | High-corrosion marine environments, liquid cooling cold plates, structural bracketry requiring elongation. |
| AlSi10Mg | 330 | 230 | 110.0 | 5.5% | Automotive EV battery housings, aerospace structural parts, high-stress robotics joint linkages. |
| A356 (T6 heat-treated) | 290 | 220 | 151.0 | 6.0% | Heavy-duty structural arms, suspension components, high-integrity pressure-tight hydraulic manifolds. |
China OEM/ODM Industrial Supply Chain Advantages
Leveraging Shenzhen and Guangdong's world-class hardware manufacturing clusters, Sunmy Hardware merges competitive toolmaking capital expenditures with high-speed engineering iteration.
1. Accelerated Tooling Lead Times
From initial DFM approval to first article inspection (FAI) sample delivery, tool fabrication takes only 15 to 25 business days using premium SKD61 or Dievar mold steel, cutting time-to-market by 40% compared to Western counterparts.
2. Fully Integrated Surface Finishing
Complete single-source control over post-injection surface treatments: CNC high-speed milling, precision bead blasting, clear/black anodizing, hardcoat anodizing, electrocoating (E-coat), and salt-spray resistant powder coating.
3. Cost-Engineering Optimization
By conducting continuous Value Engineering (VA/VE), our team optimizes wall thicknesses, gate runner designs, and mold cavities, resulting in a 20%-35% reduction in overall Total Cost of Ownership (TCO).
Strict Quality Verification & Global Regulatory Compliance
Enterprise buyers from North America, Europe, and Asia-Pacific rely on our rigorous in-house inspection standards. Every production lot is traceable to raw ingot melt batches.
Spectrometric Testing
Optical Emission Spectrometry (OES) verifies exact alloying chemical percentages before molten metal tapping.
X-Ray Defect Detection
Non-destructive industrial X-ray inspection evaluates subsurface shrinkage and porosity per ASTM E505 standards.
CMM 3D Inspection
Zeiss Coordinate Measuring Machines (CMM) record key interface tolerances down to ±0.005mm.
Salt Spray Testing
ASTM B117 salt spray chamber validation ensures surface coatings withstand over 500+ hours of harsh exposure.
Full Compliance Docs
Shipments accompanied by PPAP Level 3, FAI reports, RoHS 3, REACH SVHC, and Conflict Minerals filings.
Localized Application Scenarios across High-Tech Industries
Our custom aluminum injection casting and CNC components perform in critical operational environments worldwide.
Electric Vehicle Powertrain & Cooling
Die-cast transmission housings, inverter cold plates, motor end bells, and high-density battery tray structural frame elements designed for maximum thermal dissipation and weight reduction.
5G / 6G Outdoor RF Infrastructure
Weatherproof IP67-rated transmitter enclosures with skived or cast fin heat sinks engineered for natural convection cooling and electromagnetic interference (EMI) shielding.
High-Torque Arm Joints & Actuators
Lightweight, high-strength aluminum cast robot finger joints, swivel arms, and servo gearboxes with post-machined bearing seats engineered for backlash-free motion.
Wafer Carriers & Sleeve Bushings
Ultra-precise 8-inch wafer carriers, vacuum manifolds, and surgical equipment sleeves requiring cleanroom-ready chemical resistance and zero outgassing.
Solar Inverters & Energy Storage
Cast aluminum structural brackets and transformer heat sink enclosures built to sustain extreme atmospheric temperature swings and UV exposure.
Architectural & Ergonomic Fittings
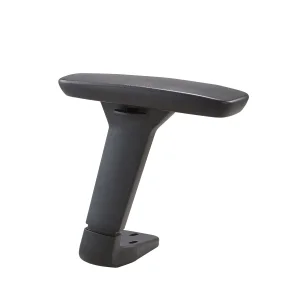
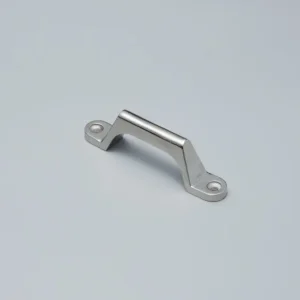
Heavy-duty structural handles, modular office chair armrests, and cast stainless/aluminum bridge handles engineered for high tactile quality and load capacity.
Emerging Trends in Aluminum Injection Casting (2026–2035)
As global industries transition toward carbon neutrality and structural electrification, three major technological shifts are revolutionizing aluminum die casting and injection processes.
1. Gigacasting & Large Integrated Castings
Moving away from stamping and welding hundreds of individual sheet metal parts, single-piece Gigacast aluminum sub-frames reduce vehicle assembly complexity, cut vehicle body weight by 20%, and reduce manufacturing footprints.
2. Green Aluminum & Recycled Alloy Ingot Integration
Adopting low-carbon primary aluminum smelted using renewable hydroelectric energy, alongside high-ratio secondary recycled alloy formulations. Reduces embedded product carbon footprint (Scope 3 emissions) by up to 70% to comply with EU CBAM directives.
3. AI-Driven Real-Time Shot Cavity Monitoring
Implementation of IoT pressure transducers and optical pyrometers inside the die cavity. AI neural networks adjust shot sleeve acceleration dynamically per cycle, guaranteeing near-zero scrap rates and perfect density.
How to Request an Accurate ODM Aluminum Injection Casting Quote
To ensure your quotation is processed within 24 hours with comprehensive DFM feedback, submit your package with the following engineering parameters.
1. 3D CAD & 2D Engineering Drawings
Provide 3D vector geometry files in .STEP, .IGES, or .X_T format alongside 2D .PDF prints detailing critical datum targets, geometric dimensioning and tolerancing (GD&T), and threaded hole callouts.
2. Material Specification & Annual Volume
Indicate required aluminum alloy grade (e.g., A380, ADC12, AlSi10Mg). State sample lot size, pilot production expectations, and estimated annual volume (EAV) to optimize mold cavity layout (single vs. multi-cavity tool).
3. Surface Coating & Secondary Operations
Specify surface finish roughness (Ra), anodizing color/thickness, powder coating specs, or leak testing parameters (e.g., 0.5 bar pressure decay helium testing for fluid housings).
Frequently Asked Questions (FAQ)
Engineering and procurement responses regarding aluminum injection casting capabilities, tolerances, tooling, and quality control.
Custom Machined & Molded OEM Component Solutions
Direct factory supply for global industrial, communication, and automotive systems.