
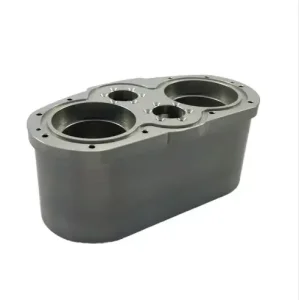
China Factory Custom 5-Axis CNC Machined Steel & Aluminum Universal Joint Base and Gearbox Shell for Robotics & Drone Industry Suppliers, Factories
View Details
ODM Universal Breathable Silicone Sport Watch Strap with Multi-Hole Air Vents (18mm - 24mm) Manufacturers, Product
View Details
ODM China Suppliers Factory Dual-Material Power Tool Handle with Two-Shot Injection Molding Technology Manufacturers, Products
View Details
High-Quality Custom CNC Machined Spur Gear & Gear Shaft from China Suppliers - High-Quality Factory Engineering Solutions Suppliers, Products
View Details
High-Quality Custom CNC Machined Carbon Fiber Drone Frame Kits | High-Performance Quad/Hexacopter Frames for Agriculture & FPV Manufacturers, Quotes
View Details
Custom High-Quality Stainless Steel Centrifugal Slurry Pump with Open Impeller - China Suppliers & Factory Product, Quotes
View Details
ODM High-Quality Centrifugal Slurry Pump with Open Impeller - Stainless Steel Suppliers and Factory in China Manufacturers, Exporter
View Details
ODM Custom Black Anodized Aluminum Lens Barrel & Optical Housing Components | China Suppliers & Factory Supplier, Quotes
View DetailsGlobal Procurement Demand & Technical Imperatives for Custom TIG Welding
An in-depth whitepaper analysis on modern Gas Tungsten Arc Welding (GTAW) fabrication, metallurgical integrity, and scalable supply chain strategies for tier-1 OEMs.
The Shifting Paradigm in Advanced Industrial Metal Joining
Gas Tungsten Arc Welding (GTAW), commonly referred to as Tungsten Inert Gas (TIG) welding, represents the pinnacle of precision metal joining technologies. Across modern global manufacturing—spanning aerospace propulsion systems, semiconductor ultra-high purity (UHP) gas delivery lines, nuclear pressure vessels, and defense-grade marine hulls—the demand for ultra-clean, structurally flawless, and metallurgically sound joints has experienced exponential growth.
Procurement teams and engineering directors from Fortune 500 companies are moving away from traditional transactional fabrication toward strategic partnerships with custom TIG welding manufacturers capable of offering integrated DFM (Design for Manufacturability), non-destructive testing (NDT), automated orbital welding, and full material traceability (EN 10204 3.1/3.2 certificates).
Information Gain Insight: Unlike MIG (GMAW) or Submerged Arc Welding (SAW), TIG welding delivers an unexcelled level of control over thermal input and weld bead geometry. This precise heat regulation minimizes Heat-Affected Zone (HAZ) expansion, prevents grain growth, and eliminates spatter, making it non-negotiable for critical thin-gage alloys, reactive metals (Titanium, Zirconium), and vacuum-tight enclosures.
Technical Matrix: TIG Welding vs. Alternative Industrial Joining Processes
When selecting a manufacturing route for mission-critical hardware, procurement officers must evaluate processes across key metallurgical and operational parameters:
| Process Parameter | Custom TIG (GTAW) | MIG (GMAW) | Fiber Laser Welding | Electron Beam (EBW) |
|---|---|---|---|---|
| Weld Aesthetics & Cleanliness | Pristine, zero spatter, scale-free | Moderate spatter, high post-cleaning | Clean, minimal oxidation | Ultra-clean, zero atmosphere contamination |
| Heat Affected Zone (HAZ) | Tightly Controlled / Micro-Pulsed | Broad / High Thermal Input | Extremely Narrow | Ultra-Narrow Deep Penetration |
| Material Compatibility | Universal (Ti, Inconel, SS, Al, Cu) | Carbon Steel, Aluminum, SS | Select Metals (Reflectivity issues) | Exotic Metals & Heavy Sections |
| Hermetic Sealing / Vacuum Spec | UHP Helium Leak Rate < 10⁻⁹ mbar·l/s | Not Suitable for High Vacuum | Excellent with Proper Purge | Superior High Vacuum Class |
| Capital / Unit Cost Profile | Medium Tooling / High Skill Efficiency | Low Tooling / Rapid Deposition | High Capital / Low Operating Cost | Ultra-High Capital (Vacuum Chamber) |
Comprehensive TIG Metallurgy Across Specialty Alloys
Mastering thermal expansion, phase transformation, and intergranular corrosion prevention across high-temperature and reactive metals.
Austenitic & Duplex Stainless Steels
Expert fabrication of 304L, 316L, 904L, Duplex 2205, and Super Duplex 2507. We utilize trailing gas shields and high-purity argon backing purges (oxygen content < 50 ppm) to eliminate sensitization, chromium carbide precipitation, and sugar-cube oxidation.
Aluminum & Magnesium Aerospace Alloys
AC TIG welding with dynamic square-wave balance control for 6061-T6, 7075, 5083, and 2024 alloys. High-frequency arc initiation ensures oxide film breakdown without tungsten inclusion, maintaining high tensile strength and structural integrity.
Refractory & Reactive Exotic Metals
Dedicated purge chambers and glovebox TIG welding for Titanium (Grades 2, 5, 7, 23), Inconel 625/718, Hastelloy C-276, and Monel 400. Full protection against interstitial embrittlement from atmospheric hydrogen, nitrogen, and oxygen contamination.
Managing Thermal Distortion & Weld Pool Fluid Dynamics
One of the primary engineering challenges in custom TIG welding of complex geometry structures is controlling thermal distortion. The non-uniform heating and cooling cycles introduce localized stresses, resulting in angular distortion, longitudinal shrinkage, and buckling in thin-walled assemblies.
Our engineering team combats thermal distortion through rigorous computer-aided thermal modeling and process controls:
- Dynamic Pulsed Current (DPC-TIG): Alternating between high peak current (for root penetration) and low background current (to allow the weld pool to solidify), reducing total heat input by 30% to 50% compared to continuous wave TIG.
- Cryogenic & Water-Cooled Fixturing: Customized copper-chilled backing bars and pneumatic clamping jigs rapidly extract thermal energy away from the heat-affected zone, maintaining tight geometrical tolerances down to ±0.1mm on large fabrications.
- Symmetrical Weld Sequencing: Utilizing dual-operator synchronized TIG or pre-programmed robotic paths to balance residual stresses across opposing structural axes.
The Convergence of AI, Robotics & Automated Orbital TIG
How cutting-edge smart sensors, machine vision, and robotic cold-wire automation are redefining precision industrial manufacturing.
Robotic 6-Axis Articulated TIG
Integration of Fanuc & KUKA robotic arms fitted with water-cooled TIG torches and high-precision cold wire feeders for 100% repeatable bead geometry.
Closed-Loop Vision Systems
Real-time optical sensors monitor weld pool geometry, arc voltage, and seam alignment, automatically adjusting amperage in milliseconds to compensate for joint gap variations.
Automated Orbital Tubing TIG
Closed-head orbital welding power supplies executing UHP tube-to-tube and tube-to-fitting joints with internal argon purge monitoring down to 1 ppm oxygen level.
AI Defect Diagnostics
Machine-learning models trained on millions of high-speed infrared images predict micro-porosity and lack of fusion defects before the component leaves the welding cell.
Specialized Shielding Gas Formulations & Purging Technology
The purity of the gas atmosphere is the single most critical factor in achieving X-ray quality TIG welds. Our facilities employ central gas distribution networks supplying Grade 5.0 (99.999% purity) Shielding Gases and customized binary/ternary gas mixtures:
Argon-Helium Mixes (Ar/He)
Adding 25% to 75% Helium elevates the ionization voltage, dramatically increasing arc temperature and heat input depth—ideal for thick aluminum plates and heavy copper heat exchangers.
Argon-Hydrogen Mixes (Ar/H₂)
Addition of 2% to 5% Hydrogen provides a reducing atmosphere that scavenges residual oxygen, accelerating travel speeds and producing ultra-bright, oxide-free beads on 300-series stainless steel.
Nitrogen-Doped Gas Shields
Controlled additions of 1% to 2% N₂ into argon backing purge gas preserves the delicate austenite-ferrite phase balance in Duplex and Super Duplex stainless steel weld metals.
International Standards, NDT Testing & Industry Applications
Meeting the stringent quality management frameworks of ISO, ASME, AWS, and EN standards for worldwide OEM export.
Aerospace & Defense
Specification compliance under AWS D17.1 / EN 9100. Fabrication of ducting systems, titanium hydraulic lines, engine exhaust nozzles, and structural airframe bracketry with 100% Radiographic Testing (RT) requirements.
Semiconductor & UHP Systems
Orbital TIG welding of 316L VAR/VIM stainless steel tubing and gas boxes. Surface roughness of internal weld bead maintained below Ra 0.25 µm (10 µin) after electropolishing, verified via video borescope inspection.
Nuclear & High-Pressure Vessels
Welding Procedures Qualified (WPS / PQR) to ASME Section IX and EN ISO 15614-1. Full penetration butt joints subjected to Phased Array Ultrasonic Testing (PAUT) and hydrostatic pressure testing.
In-House Quality Control Protocol & NDT Verification Framework
Every single batch produced at our manufacturing plants passes through a rigid 6-stage Quality Control gate before export packaging:
1. Raw Material PMI
Positive Material Identification (PMI) using handheld XRF analyzers to confirm elemental chemical composition before torch touches metal.
2. Liquid Penetrant (PT)
Fluorescent dye penetrant inspection under ultraviolet light to detect surface-breaking cracks, pinholes, or lack of sidewall fusion.
3. Helium Mass Spec Leak
Vacuum envelope testing capable of detecting micro-leaks down to 1 x 10⁻¹⁰ std cc/sec Helium for UHP vessels and vacuum chambers.

China Custom Aluminum Optical Breadboard - Precision CNC Machining by China Suppliers & Factory Suppliers, Service
View Details
OEM Dual-Material Power Tool Handle Supplier, Products
View Details
China High-Performance Square Aluminum & Copper Skived Fin Heat Sinks from China Suppliers and Factory for LED & Industrial Electronics Service, Quotes
View Details
High-Quality China Aluminum Die-Cast Transmission Housing: Precision CNC Machining by Leading Suppliers and Factory Manufacturers, Exporter
View Details
China Premium 8-Inch CNC Machined Aluminum Semiconductor Wafer Carrier from China Suppliers - Quality Factory Manufacturing Suppliers, Factories
View Details
China Custom OEM Wheel Hub Sand Casting by Reputable China Suppliers and Factory Service, Factories
View Details
ODM Custom Aluminum Electronic Enclosure Suppliers, Products
View Details
Custom Electrical Component Metal Stamping Housings | Deep Drawn Housings for Fuses, Contactors, and Terminals Manufacturers, Product
View DetailsFrequently Asked Questions (FAQ) for OEM Buyers
Detailed engineering responses regarding manufacturing capabilities, quality documentation, MOQs, and global export compliance.