
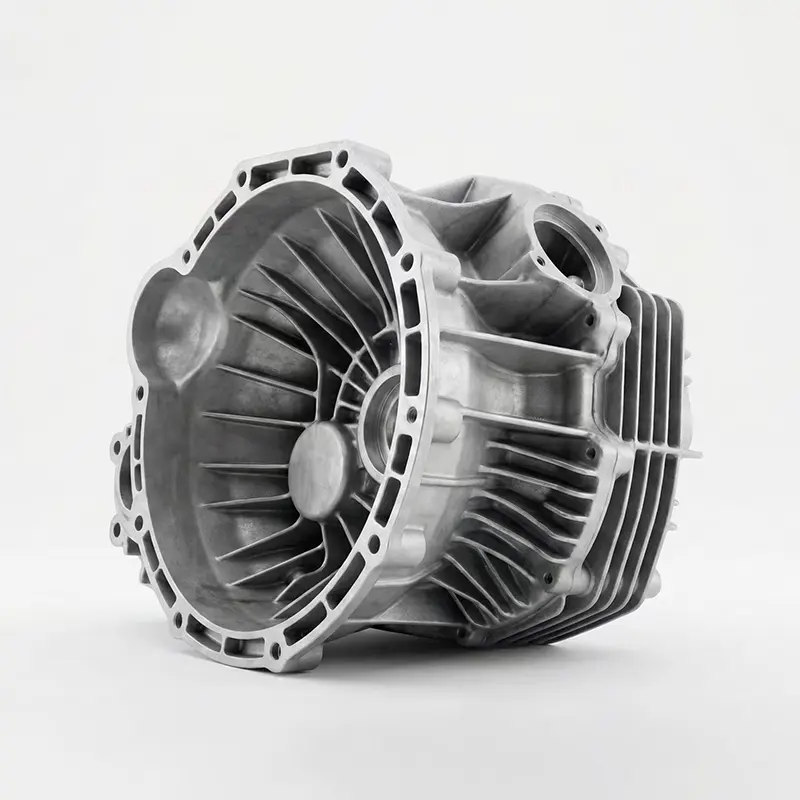
High-Quality China Aluminum Die-Cast Transmission Housing: Precision CNC Machining by Leading Suppliers and Factory Manufacturers, Exporter
Product Description
Product Overview
This complex aluminum housing is a key component for automotive transmission systems. It demonstrates Sunmy Hardware's capability to manage complex geometries that require both lightweight characteristics and high structural strength. This project highlights our expertise in bridging the gap between raw casting and precision post-machining.
Key Specifications
| Material | Aluminum Alloy ADC12 |
| Process | High-Pressure Die Casting (HPDC) + CNC Milling |
| Weight | 2.5 kg |
| Mold Cavity | 1*1 |
| Surface Treatment | Shot Blasting |
Manufacturing Process Insight
Mold Flow Analysis
Before production, we simulate the filling process to optimize gate locations, minimizing porosity and air pockets.
High-Pressure Die Casting (HPDC)
We use a 400T cold chamber die casting machine with ADC12 aluminum alloy to form the complex shape, including the thin cooling fins.
Precision Post-Machining
After casting, the part is transferred to a 4-axis CNC machining center. We mill the mating surfaces and bore the bearing holes to H7 tolerance, ensuring perfect assembly alignment.
Key Features & Benefits

Thermal Management
Integrated cooling fins maximize surface area for rapid heat dissipation, critical for protecting internal gears.

Weight Reduction
Optimized wall thickness reduces overall vehicle weight without compromising durability.

Complex Internal Structure
Includes cast-in ribs and bosses that would be too costly to produce via machining alone.

Surface Treatment
Shot blasting removes flash and burrs, providing a uniform matte texture ready for assembly or painting.
Technical FAQ
▶ Q1: What is the typical mold life?
A1: Our high-quality tool steel molds (H13) typically last for 50,000 to 100,000 shots depending on maintenance.
▶ Q2: Can you control porosity in the casting?
A: Yes, through vacuum-assist die casting and strict parameter control, we minimize porosity to meet automotive standards.
▶ Q3: Do you offer leak testing?
A3: Absolutely. We can design custom fixtures to perform air decay leak testing on every housing.
Other Products
Custom SS316 Deep Drawn Closed-End Flanged Sensor Housing for Temperature Probes (4mm OD)
Custom Tinned Copper Lug Ring Crimp Terminal Battery Wire Connector & Metal Stamping Brass Plug
Custom Laser Cut & Welded Heavy Equipment Control Panel
Custom Phosphor Bronze and Steel Stamping Battery Contacts for AG13, CR2032, and CR2450 Coin Cells
Get a Fast, Technical Quote & Free DFM Review
Don't let tolerance stack-up delay your product launch. Submit your project details, and our engineering team will evaluate your design for manufacturability before the first cut.
Frequently Asked Questions
-
QWhat aluminum alloy is used for this transmission housing, and why?
We use ADC12 aluminum alloy, which offers an excellent balance of fluidity, strength, and corrosion resistance. It is the industry-standard choice for high-pressure die casting of automotive structural components.
-
QWhat tolerances can you achieve on the machined features?
Our 4-axis CNC machining center can achieve tight tolerances on critical features such as bearing bores to H7 tolerance and mating surfaces to within ±0.02mm, ensuring perfect assembly alignment.
-
QWhat is the minimum order quantity (MOQ) for this type of die casting part?
MOQ depends on the complexity and tooling investment. For automotive-grade die cast housings, we typically recommend a minimum of 500 pieces per order to ensure cost-effectiveness, but we are happy to discuss your specific project requirements.
-
QCan this housing be further surface-treated beyond shot blasting?
Yes. While shot blasting provides a clean, uniform matte finish ready for assembly or painting, we can also arrange additional surface treatments such as anodizing, powder coating, or chemical film coating based on your application requirements.
-
QHow do you ensure dimensional consistency across large production runs?
We implement a rigorous quality control process including First Article Inspection (FAI), in-process CMM measurement, and statistical process control (SPC). Each batch is verified against your approved drawings before shipment.
-
QWhat is the typical lead time from tooling approval to mass production delivery?
After mold design and DFM approval, tooling fabrication typically takes 4–6 weeks. Once the mold is approved via T1 samples, mass production lead time is generally 3–5 weeks depending on order volume and finishing requirements.









