
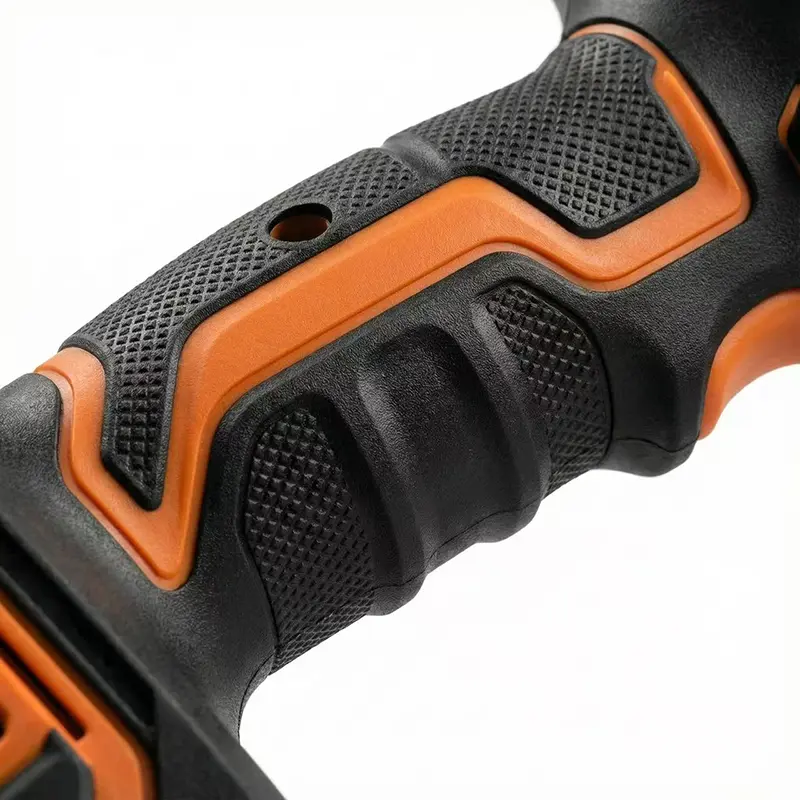
ODM China Suppliers Factory Dual-Material Power Tool Handle with Two-Shot Injection Molding Technology Manufacturers, Products
Product Description
ⓘ Product Overview
This ergonomic handle demonstrates our advanced capabilities in multi-material injection molding. By combining a rigid substrate with a soft-touch grip, we enhance both the durability and the user experience of the product. This technology is widely used in power tools, consumer electronics, and outdoor equipment.
⚙ Manufacturing Process Insight
Overmolding Technique
First, the rigid core (Glass-filled Nylon) is molded to provide structural strength. Then, the part is transferred to a second cavity (or using a 2K machine) where soft TPE (Thermoplastic Elastomer) is injected over it.
Chemical Bonding
We select materials that chemically bond during the molding process, eliminating the need for adhesives and preventing peeling over time.
Complex Tooling
The mold is designed with precise shut-offs to ensure the soft material creates crisp, clean lines without flashing onto the hard plastic.
★ Key Features & Benefits

Ergonomics
The TPE layer provides vibration dampening and a non-slip grip, improving user comfort.

Aesthetics
Enables dual-color designs that enhance brand identity and shelf appeal.

Durability
The glass-filled nylon core creates a nearly unbreakable internal skeleton.

Cost Efficiency
Two-shot molding eliminates manual assembly of rubber grips, reducing labor costs in mass production.
? Technical FAQ
A1: Common combinations include ABS+TPE, PC+TPU, or Nylon+TPE. Material compatibility is key for chemical bonding.
A: Double-shot molds are more complex and costly than single-shot molds, but the unit price is lower for high-volume production due to eliminated assembly steps.
A3: Yes, we can robotically place brass nuts or metal shafts into the mold before injection.
📦 Other Products
✉ Get a Fast, Technical Quote & Free DFM Review
Don't let tolerance stack-up delay your product launch. Submit your project details, and our engineering team will evaluate your design for manufacturability before the first cut.
💡 Frequently Asked Questions
Overmolding is a two-step injection molding process where a second material (typically a soft TPE or rubber) is molded over a pre-formed rigid substrate. Unlike standard single-shot injection molding, overmolding combines two different materials into one integrated part without adhesives or mechanical fasteners, resulting in a stronger, more ergonomic product.
MOQ varies depending on part complexity, tooling investment, and material selection. Generally, overmolded components are most cost-effective for production runs of 1,000 units or more. We can discuss prototype or low-volume options using alternative tooling strategies — please contact our team for a tailored quote.
Tooling lead time for a two-shot or overmolded mold typically ranges from 4 to 8 weeks, depending on part complexity and mold design requirements. We provide a detailed project timeline after reviewing your DFM (Design for Manufacturability) analysis and finalizing the mold design.
Yes. We work with customer-specified materials and can source custom color-matched compounds. Our engineering team will verify material compatibility for chemical bonding to ensure the overmolded layers adhere correctly throughout the product's service life.
We offer a wide range of mold surface finishes including SPI standards (A1 to D3), custom textures (diamond, leather grain, fine matte), and logo or pattern embossing. Texture selection impacts both aesthetics and grip performance, and our team can advise on the best option for your application.
Yes. We provide full dimensional inspection reports (PPAP available upon request), material certifications (RoHS, REACH compliance), and process control documentation. Each production batch undergoes in-process quality checks, and we can arrange third-party inspection if required by your supply chain standards.









