
Featured CNC & Precision Component Portfolio
Explore our top-tier manufactured OEM components, engineered to micrometric tolerances for international B2B clients.

China Custom Precision Injection Molded POM Plastic Gears Manufacturers, Products
View Product Specifications
China High-Performance Hydraulic Solenoid Valve Core - Precision CNC Turned Excavator Parts
View Product Specifications
High-Quality China Custom Tinned Copper Lug Ring Crimp Terminal Battery Wire Connector
View Product Specifications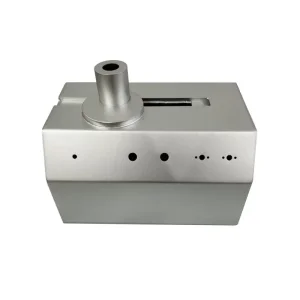
ODM Custom Precision Sheet Metal Equipment Enclosure Manufacturer, Supplier
View Product Specifications
ODM Custom Precision CNC Machined Aluminum Hinge Assembly Structural Connector
View Product Specifications
ODM Custom Phosphor Bronze and Steel Stamping Battery Contacts for AG13, CR2032, CR2450
View Product Specifications
OEM Custom CNC Turned Titanium Abutment Implant Driver & Prosthetic Connector
View Product Specifications
China Custom Aluminum Optical Breadboard - Precision CNC Machining by China Suppliers
View Product SpecificationsThe Paradigm Shift in Global CNC Bicycle Component Manufacturing
How advanced Chinese precision machining hubs are redefining weight-to-strength ratios, kinematic reliability, and OEM manufacturing agility for tier-1 cycling brands.
The global cycling industry is experiencing an unprecedented structural transformation. Driven by the rapid proliferation of Electric Bicycles (E-bikes, EPACs), high-performance gravel bikes, downhill mountain bicycles (MTB), and ultra-lightweight road race platforms, the technical demands placed on component manufacturing have escalated exponentially. Modern bicycle architectures require mechanical elements that balance dynamic stress distribution, high torsional rigidity, rotational inertia optimization, and absolute micro-metric fatigue resistance.
Historically, high-volume bicycle hardware relied on gravity die casting or standard cold forging. However, modern kinematic engineering demands intricate geometries, internal weight-reduction pockets (thin-wall structures down to 0.8 mm), and strict dimensional stability under sustained torque loading. High-precision CNC machining (Computer Numerical Control)—utilizing multi-axis milling, Swiss-type lathe turning, and hybrid subtractive manufacturing—has emerged as the foundational manufacturing methodology for mission-critical components.
Mapping Global Enterprise Sourcing Intent for CNC Bike Components
Analyzing the primary engineering pain points, material parameters, and manufacturing specifications requested by European, North American, and Asian OEM procurement teams.
E-Bike Drive Unit & Motor Interface Mounts
Mid-drive motor brackets (compatible with Bosch, Shimano STEPS, Bafang systems) require extreme stiffness to transmit sustained electric motor torques up to 90 Nm without rotational deflection. We CNC machine multi-point mounting plates with sub-hundredth millimeter hole alignment.
Precision Drivetrain & Cassette Architecture
Direct-mount chainrings, narrow-wide tooth profiles, and 12-speed monoblock cassette cogs demand high 5-axis milling accuracy to prevent chain drop, optimize wear patterns, and maximize energy transfer efficiency across dynamic angular vectors.
Hydraulic Brake Calipers & Master Cylinders
Monoblock 4-piston disc brake calipers turned and milled from solid AL6061-T6 or AL7075-T6 billets. Internal hydraulic fluid channels require mirror-like surface finishes (Ra 0.4 µm) to ensure perfect Quad-Ring sealing under extreme thermal pressure.
Suspension Linkages & Pivot Assemblies
Full-suspension MTB rocker arms and rear triangle links require 3D organic pocketing to shed weight while maintaining lateral rigidity. Precise bearing seats bored to H7 tolerance guarantee play-free suspension articulation.
Custom Hubs, Freehub Bodies & Axles
Precision Swiss-turned 7075-T6 aluminum hubs and high-engagement ratchet systems. Features precise thread pitch control, micro-spline interfacing, and anodized corrosion protection for thru-axle standards.
Stem Clamps, Headset Spacers & Seat Posts
Ergonomic, featherlight cockpit components. Machined with Chamfered edge profiles, custom laser-etched alignment graphics, and stress-relieved geometry to prevent carbon fiber steerer tube crushing.
Technical Roadmap: Alloys, Machining & Surface Treatment
Comprehensive breakdown of raw material selection criteria, machining protocols, and anti-corrosive finishing processes optimized for heavy outdoor cycling stress.
1. Advanced Substrate Metallurgy
Selecting the optimal material substrate is paramount when balancing tensile yield strength against volumetric mass. Sunmy Hardware manufactures CNC components from certified mill-grade raw stock:
| Material Standard | Tensile Strength (MPa) | Yield Strength (MPa) | Hardness (HB) | Primary Bicycle Component Application |
|---|---|---|---|---|
| AL7075-T6 Aluminum | 572 MPa | 503 MPa | 150 HB | Cassettes, Chainrings, Suspension Linkages, Stem Bodies |
| AL6061-T6 Aluminum | 310 MPa | 276 MPa | 95 HB | Brake Caliper Housings, Seat Clamps, Hub Shells, Pedals |
| Titanium Ti-6Al-4V (Grade 5) | 950 MPa | 880 MPa | 36 HRC | Fasteners, Thru-Axles, Pedal Spindles, Custom Frame Bosses |
| Stainless Steel 316 / 17-4 PH | 750–1100 MPa | 550–1000 MPa | 25-38 HRC | Hydraulic Valve Pistons, Disc Rotor Fasteners, Bearings |
| POM-C (Polyacetal / Delrin) | 70 MPa | 65 MPa | 85 R scale | Internal Cable Guides, Derailleur Pulley Wheels, Bushings |
2. Precision Surface Finishing & Tactical Coatings
Bicycle components operate under relentless exposure to moisture, road salt, mud, UV radiation, and kinetic abrasion. To maximize service lifespan, Sunmy Hardware provides comprehensive surface treatment solutions executed under strict process controls:
- Type III Hard Anodizing (MIL-A-8625): Creates a ceramic-like aluminum oxide layer (thickness 25–50 µm) with extreme surface hardness (up to 400–500 HV). Crucial for suspension stanchions, chainring teeth, and high-wear pivot points.
- Type II Color Anodizing: Offers vibrant architectural aesthetic finishes (Black, Oil Slick Cyan, Bronze, Violet) with excellent corrosion protection and UV resistance for consumer-facing aftermarket components.
- Physical Vapor Deposition (PVD): Applies Titanium Nitride (TiN), Titanium Carbonitride (TiCN), or Diamond-Like Carbon (DLC) coatings onto titanium and steel components, dropping friction coefficients below 0.1 while enhancing visual appeal.
- Precision Bead Blasting & Electropolishing: Media blasting with glass beads (100–170 mesh) provides uniform satin matte finishes, hiding minor directional tooling marks prior to anodizing.
Factory Floor Infrastructure & Quality Verification
Shenzhen Sunmy Hardware Co., Ltd. integrates direct-factory production efficiency with stringent laboratory-grade quality controls.
Advanced Multi-Axis CNC Milling
Equipped with high-speed 3, 4, and 5-axis machining centers featuring 20,000 RPM spindles. We efficiently execute complex 3D contouring, deep pocketing, and single-setup multi-sided operations.
Swiss-Type Lathe Turning
Dedicated high-precision Swiss automatic lathes for high-volume rotational components including titanium bolts, hydraulic brake hose inserts, thru-axles, and cassette spacers with sub-micron repeatable precision.
In-House CMM & FAI Verification
Our quality lab utilizes Zeiss Coordinate Measuring Machines (CMM), optical profile projectors, thread pitch micrometers, and surface roughness testers. Full First Article Inspection (FAI) reports included with production shipments.
Founded in 2016 in Longgang District, Shenzhen, Sunmy Hardware works directly with global OEM buyers. By keeping DFM engineering reviews, programming, CNC machining, metal stamping, and dimensional inspection in-house, we eliminate broker markups and guarantee strict intellectual property protection under NDA protocols.
Compliance Framework & International Supply Chain Security
Ensuring full technical compliance with global bicycle safety directives, environmental standards, and cross-border logistics fulfillment.
International Bicycle Standards Adherence
Bicycle parts manufactured by Sunmy Hardware are engineered to meet or exceed rigorous mechanical stress testing standards:
- ISO 4210: Safety requirements for city, trekking, mountain, and racing bicycles (fatigue tests, dynamic impact load testing).
- EN 15194 (EPAC): Specific structural safety parameters tailored for high-speed Electrically Power Assisted Cycles.
- REACH & RoHS Compliance: Surface treatments, plating, and anodizing colors contain no restricted hazardous chemical substances.
End-to-End Fulfillment & IP Safeguards
Navigating international procurement requires seamless administrative efficiency and absolute design confidentiality:
- Ironclad Non-Disclosure Agreements: Formal NDA signed prior to collecting any STEP, IGES, or CAD native files.
- Complete Material Traceability: Raw material heat numbers and original steel/aluminum mill test certificates provided.
- Flexible Incoterms Support: DDP (Delivered Duty Paid), FOB Shenzhen, CIF, or EXW options with custom export-grade packaging.
Frequently Asked Questions (FAQ) for OEM Buyers
Detailed technical answers to common queries regarding CNC machining tolerances, lead times, material selections, and order scaling.
What precision tolerances can Sunmy Hardware hold for custom CNC bicycle components?
Our standard CNC machining tolerance is ±0.01 mm. For critical bearing interfaces, hydraulic caliper cylinder bores, and bottom bracket press-fit surfaces, our 5-axis machining centers and Swiss lathes can hold tight tolerances down to ±0.005 mm (5 microns). All precision dimensions are documented via CMM inspection before release.
Why should we choose CNC machined aluminum over forged aluminum for bike parts?
While forging offers high grain alignment for high-volume basic shapes, CNC machining provides unmatched geometrical freedom, enabling complex internal weight-reduction pockets, organic 3D shapes, and rapid DFM iterations without requiring thousands of dollars in upfront forging dies. For low-to-medium volumes or premium lightweight aftermarket components, CNC billet machining delivers superior flexural control and aesthetic crispness.
How do you ensure color consistency across large anodized batches of bicycle hardware?
Color consistency in Type II anodizing requires strict control over aluminum alloy composition, bath temperature, current density, dye bath immersion times, and sealing chemical balances. Sunmy Hardware uses single-source certified aluminum billets for each production run and utilizes spectrophotometer color-matching technology to keep batch-to-batch variation within Delta E < 1.0.
Can you manufacture custom titanium bicycle components, such as thru-axles or pedal spindles?
Yes. We regularly machine Titanium Grade 5 (Ti-6Al-4V) using dedicated high-rigidity CNC turning centers and specialized tooling. Titanium offers an extraordinary strength-to-weight ratio and natural corrosion resistance, making it ideal for high-stress fasteners, lightweight axles, and custom frame hardware.
What is your typical turnaround time for rapid prototypes versus mass production runs?
Rapid CNC prototypes (1 to 10 pieces) are typically manufactured, inspected, and surface-finished within 3 to 7 business days. Full production orders (500 to 10,000+ pieces) generally take 15 to 25 business days depending on surface finishing complexity (such as multi-color anodizing or laser marking requirements).
How do we initiate a custom manufacturing RFQ with your engineering team?
You can send your 3D CAD files (STEP, IGES, X_T formats) alongside 2D technical drawings (PDF format with annotated tolerances and threads) directly to [email protected]. Our engineering team reviews all files for Manufacturability (DFM) and returns a comprehensive quotation with unit pricing, tooling suggestions, and production timelines within 24 hours.
Additional OEM Hardware & Precision Assemblies
Browse our extended product portfolio spanning sheet metal enclosures, capillary tubing, custom hinges, and turned connectors.

OEM China OEM ODM 1U Rackmount Server Chassis (Model 1U25- Custom Mini-ITX Metal Enclosure)
View Product Specifications
OEM Custom Precision Capillary Stainless Steel Pipe / Tube 1mm - 8mm | China Suppliers
View Product Specifications
ODM OEM ODM 1U Rackmount Server Chassis (Model 1U25- Custom Mini-ITX Metal Enclosure)
View Product Specifications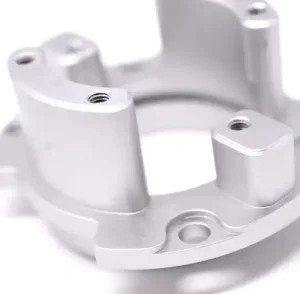
ODM Precision 5-Axis CNC Machined Aluminum Housing Mounting Bracket for Aerospace
View Product Specifications
Custom Custom Laser Cut Heavy Equipment Control Panels - China Suppliers & Factory Products
View Product Specifications
China Premium Custom Stainless Steel Casting Factory - Suppliers of Water Valves & Impellers
View Product Specifications
OEM Custom Plastic Injection Molded Control Knob with Brushed Metallic Finish
View Product Specifications
OEM Custom Precision Sheet Metal Brackets & Stamping Parts for Electronic Devices
View Product SpecificationsReady to Accelerate Your CNC Bicycle Parts Production?
Submit your CAD files today for a 24-hour Design for Manufacturability (DFM) review and comprehensive price quotation from our senior engineering team.