Featured Precision Components & Assemblies
Direct factory production spanning semiconductor wafer carriers, automotive retarder pans, hydraulic cast fittings, and sub-micron turned turned parts.
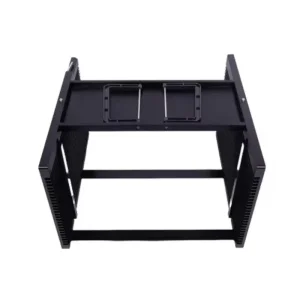
China Premium 8-Inch CNC Machined Aluminum Semiconductor Wafer Carrier Manufacturer, Exporter
Request Specifications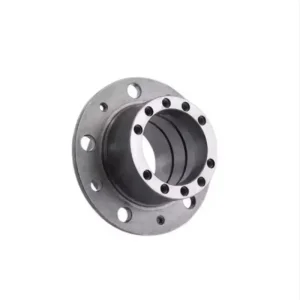
OEM Custom OEM Iron & Steel Sand Casting Wheel Hub Suppliers, Exporter
Request Specifications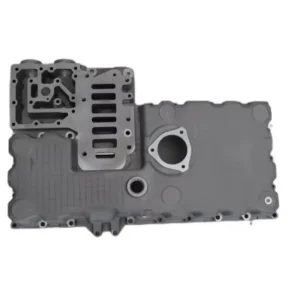
OEM Premium Automotive Transmission Retarder Engine Low-Pressure Cast Aluminum Alloy Clutch Oil Pan Exporters, Quotes
Request Specifications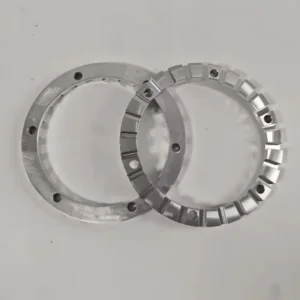
ODM Custom Anodized Sealing Rings for Semiconductor & Optical Instruments - China Factory Suppliers Manufacturers, Quotes
Request Specifications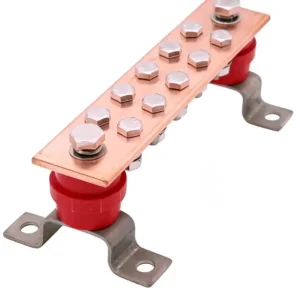
High-Quality Custom High-Conductivity Copper Grounding Busbar Kit with Stand-off Insulators Manufacturer, Factory
Request Specifications
ODM China Suppliers Premium 8-Inch CNC Machined Aluminum Semiconductor Wafer Carrier from Top Factory Suppliers, Manufacturers
Request Specifications
Custom OEM Precision CNC Machining Aluminum Parts - Custom Industrial Components from China Suppliers & Factory Service, Factory
Request Specifications
OEM Premium Custom Stainless Steel Casting Services Water Valves, Impellers, Pipe Fittings & Lugs Manufacturer, Product
Request SpecificationsThe Commercial Landscape of Global Screw Machining
From mechanical cam-driven automatics to 13-axis CNC Swiss sliding headstock centers, screw machining remains the linchpin of high-volume, micro-rotational component manufacturing.
Evolution of High-Throughput Turning
Screw machining originated with mechanical screw lathes designed for continuous fastener production. Today, the sector has evolved into ultra-complex multi-axis CNC Swiss turning centers capable of complete, single-setup machining of parts featuring cross-holes, eccentric milling, threading, and back-end deburring with zero secondary handoffs.
- Simultaneous dual-spindle processing cutting cycle times by 65%
- Sliding headstocks supporting high length-to-diameter ratios without deflection
Global Market & Supply Chain Shifts
Global industrial procurement managers face recurring bottlenecks in domestic European and North American machine shops, characterized by aging machinist labor, long tooling lead times, and prohibitive hourly machine rates ($120–$180/hr). Sourcing teams are turning toward integrated Asian manufacturing clusters for responsive capacity.
- Lower capital hurdle for prototype-to-production tooling handoffs
- Comprehensive in-region raw bar stock supply chains (SS316L, 17-4PH, Brass, Titanium)
Demands for Extreme Tolerance Control
As consumer tech miniaturizes and medical interventions become less invasive, screw machining suppliers are held to geometrical dimensioning and tolerancing (GD&T) standards below ±0.005 mm (5 microns), necessitating climate-controlled workshops, real-time laser tool wear monitoring, and automated optical batch sorting.
- Statistical Process Control (SPC) with CPK values exceeding 1.67
- Cryogenic and high-pressure through-coolant chip evacuation
China Factory Ecosystem: The Shenzhen Engineering Advantage
The Greater Bay Area (Guangdong-Hong Kong-Macao) offers an unmatched industrial concentration where metal stock, custom carbide tooling, heat treatment, and precision electroplating operate within a 30-mile radius.
Compressed Tooling Cycles
Where Western counterparts require 8–12 weeks to schedule production fixtures and source specialized collets or carbide form tools, Shenzhen facilities fabricate in-house custom jigs within 72 hours, accelerating FAI (First Article Inspection) sample dispatch to under 7 business days.
Vertical Integration under One PO
Screw machining rarely lives in isolation. OEM hardware requires integrated passivating, electroless nickel plating, case hardening, PVD coating, or precision micro-stamping. Our Shenzhen manufacturing network completes entire multi-process BOM assemblies under a single consolidated purchase order.
Skilled Technical Workforce
Our engineers possess deep knowledge of CAM programming (Mastercam, ESPRIT, Siemens NX) tailored to multi-axis Swiss kinematics. Continuous shop floor optimization minimizes cycle times, eliminates redundant air-cuts, and ensures steady burr-free microscopic edge breaks.
Transparent Raw Material Traceability
Direct partnerships with certified domestic and imported metal mills ensure every lot of rod, wire, and extruded profile comes accompanied by certified chemical composition and tensile mill test reports (MTR), matching ASTM, DIN, JIS, and AMS specifications.
Process Comparison: Swiss CNC vs. Multi-Spindle Automatics vs. Standard CNC Turning
Selecting the appropriate screw machining discipline depends on batch scale, aspect ratio, geometric complexity, and allowable per-unit unit cost.
| Evaluation Metric | Swiss CNC Screw Machining | Multi-Spindle Automatics | Conventional CNC Lathe / Turning |
|---|---|---|---|
| Typical Diameter Range | Ø 0.5 mm to Ø 38 mm | Ø 3.0 mm to Ø 65 mm | Ø 10 mm to Ø 350+ mm |
| Part Aspect Ratio (L/D) | Up to 30:1 (Guided by bushing) | Typically < 6:1 | Typically < 4:1 without tailstock |
| Standard Tolerance Range | ±0.005 mm (0.0002") | ±0.025 mm (0.0010") | ±0.015 mm (0.0006") |
| Economic Batch Threshold | 500 to 100,000+ units | 50,000 to 5,000,000+ units | 1 to 2,500 units |
| Simultaneous Machining Axis | 7 to 13 Axes with Live Tooling | Mechanical Cams / 4 to 8 Spindles | 2 to 4 Axes (Live milling optional) |
| Setup Time & Changeover | Moderate (2–4 hours) | Extended (8–24 hours) | Rapid (30–90 minutes) |
| Ideal Component Typology | Long pins, shafts, micro-valves, dental studs | High-volume automotive fasteners, bushings | Large flanges, pump impellers, disk hubs |
Engineered Applications Across Mission-Critical Verticals
From subsea optical hermetic connectors to high-vacuum semiconductor handling arms, custom screw machined components guarantee zero-fail integrity.
Semiconductor & Optoelectronics
Cleanroom-ready components including wafer chuck vacuum pins, gas distribution manifold nozzles, optical fiber ferrules, and hermetic sensor housings machined from stainless 316L, Kovar, and Invar. Strict Ra 0.2 µm polishing prevents particulate buildup in dry etch or photolithography chambers.
Automotive ADAS & Powertrain
High-speed turning for ABS/ESC brake hydraulic valve spools, fuel injector metering pins, variable valve timing (VVT) shafts, and electric drive transmission oil fittings. Fully serialized manufacturing lines support PPAP Level 3 documentation with heat-treat induction hardened cores.
Medical & Surgical Instrumentation
Titanium Grade 5 (Ti-6Al-4V ELI) and PEEK orthopedic bone screws, dental implant abutments, catheter guide tips, and endoscopic surgical scissor hinges. Burr-free ultrasonic cleaning and electrochemical deburring guarantee bio-compatible surface conditions.
High-Frequency RF & Electronics
Gold-plated brass and beryllium copper spring-loaded Pogo pins, coaxial SMA/SMP connector shells, blind-mate contact jacks, and heat dissipation copper busbar stand-offs. Controlled concentricity under 0.008 mm preserves signal integrity across GHz frequency bands.
Hydraulics, Pneumatics & Fluid Handling
Stainless 304/316 and brass hydraulic hose barbs, high-pressure check valve seats, pilot regulator poppets, and custom banjo bolts designed to resist continuous operating pressures exceeding 6,000 PSI without thread deformation.
Robotics & Motion Control
Precision stepped shafts, harmonic drive input splines, planetary gear pins, and miniature bearing races engineered for low-backlash robotic joints and drone gimbal actuators, balancing weight reduction with torsional rigidity.
Global Sourcing Requirements: Mitigating Risk in High-Volume Runs
Leading OEM buyers from North America and Europe demand auditable quality gates to prevent line-down incidents at automated assembly plants.
Metrology & In-Line Inspection
Our quality control lab utilizes multi-sensor CMMs (Zeiss / Mitutoyo), Keyence high-speed optical profile projectors, roundness testers, and MarSurf stylus profilometers. All critical features are tracked via automated run charts to monitor dimensional shift before parts breach control boundaries.
PPAP & Traceability Protocols
For series automotive and industrial programs, Sunmy Hardware implements standardized Production Part Approval Process (PPAP) Level 3 documentation, comprising Design FMEA, Process Flow Diagrams, Process FMEA, Control Plans, Gage R&R studies, and Full Dimensional FAI results per AS9102.
IP Protection & Direct Engagement
Global buyers frequently lose IP integrity and pay inflated margins when dealing with trading intermediaries. We execute legally binding bilateral Non-Disclosure Agreements before CAD reception and provide factory-direct engineering consultations, safeguarding customer proprietary geometry.
Technological Trajectories: Lights-Out Turning & AI-Driven Quality
Modern screw machining is being revolutionized by automation, automated palletizing bar feeders, and predictive cutting telemetry.
Lights-Out Unattended Production
Integrating 12-foot hydrodynamic hydrostatic bar feeders with robotic part ejectors allows our Swiss CNC cells to execute continuous 24-hour lights-out shifts. Automatic broken-tool detection sensors immediately shut down spindles in case of insert failure, preventing batch scrappage.
Adaptive Tool Wear Compensation
Contactless laser tool setters continuously measure micro-wear on turning inserts during cycle transitions. The CNC controller dynamically compensates tool offset registers in real time, eliminating human offset entry errors and sustaining consistent Cp/Cpk performance over 100,000-piece runs.
Micro-Machining & Exotic Alloys
As demand surges for biocompatible and high-temperature alloys, we utilize ultra-high-pressure (2000 PSI) through-spindle coolant delivery to machine difficult materials like Hastelloy C-276, Monel, Inconel 718, and pure Molybdenum without thermal hardening or premature tool fracturing.
Specialty Components & Industrial Hardware
Browse our extended manufacturing capabilities including precision stamped battery terminals, overmolded handles, CNC composite frames, and high-wear pump assemblies.
Custom High-Performance Custom CNC Machined Carbon Fiber Drone Frames for Agriculture & FPV | China Suppliers & Factory Supplier, Exporters
Request Specifications
Custom Custom Stainless Steel Mounting Bracket Factories, Factory
Request Specifications
OEM Dual-Material Power Tool Handle Supplier, Products
Request Specifications
OEM Custom Phosphor Bronze and Steel Battery Contacts for AG13, CR2032, CR2450 Coin Cells - China Suppliers Factory Manufacturers, Factory
Request Specifications
China Custom TPE and ABS Double Color Injection Molding & Overmolding Supplier, Manufacturers
Request Specifications
OEM China OEM Precision CNC Machining Aluminum Parts & Custom Industrial Components Supplier | Trusted Factory Products, Product
Request Specifications
ODM Universal Breathable Silicone Sport Watch Strap with Multi-Hole Air Vents (18mm - 24mm) Manufacturers, Product
Request Specifications
Custom High-Quality Stainless Steel Centrifugal Slurry Pump with Open Impeller - China Suppliers & Factory Product, Quotes
Request SpecificationsFrequently Asked Questions for Sourcing Directors & Lead Engineers
Clear, technically explicit guidance addressing common inquiries on design rules, tolerance validation, logistics, and material certifications.
What is the true distinction between custom screw machining and conventional CNC turning?
What are the minimum and maximum diameter capacities in your machining cells?
How does Sunmy Hardware guarantee roundness and concentricity on precision turned shafts?
Which documentation and quality reports are delivered with production shipments?
What are your typical prototype and mass-production lead times?
Can you machine non-standard or proprietary customer materials?
Optimize Your Turned Component Sourcing Today
Submit your 2D engineering drawings (PDF/DWG/DXF) and 3D CAD files (STEP/IGES) for a thorough Design for Manufacturability (DFM) review and competitive, volume-tiered quotations within 24 hours.