
High-Precision Metal & Polymer Integrated Solutions
Explore our export-grade custom manufactured parts engineered to sub-hundredth millimeter tolerances for robotics, electronics, automotive, and industrial hardware.








Advanced Plastic Mold Design & Manufacturing Architecture
How China's leading injection mold factories combine rheological simulation, specialized metallurgy, and micrometer-level machining to solve complex volumetric deformation.
1. The Engineering Paradigm Shift in China Plastic Mold Manufacturing
In modern industrial manufacturing, plastic mold design has evolved far beyond basic cavity cutting. As OEM hardware requirements across North America, Europe, and Asia demand ultra-tight tolerance thresholds (often down to ±0.005 mm), Chinese mold manufacturers have transitioned into comprehensive engineering partners. Modern plastic tooling requires a multi-physics approach encompassing thermal kinetics, polymer rheology, structural mechanics, and high-speed CNC finish-machining.
At Shenzhen Sunmy Hardware Co., Ltd., our engineering protocol begins long before steel hits the mill. Utilizing high-resolution Moldflow CAD/CAE simulations, our engineering team evaluates volumetric shrinkage, shear stress distribution, cooling channel efficiency, and gate placement. By accurately predicting potential defects—such as weld line degradation, sink mark formation, and differential thermal warpage—we eliminate costly tool modifications prior to steel hardening.
2. Tool Steel Metallurgy & Thermal Management Matrix
The operational lifespan, cycle efficiency, and surface fidelity of a plastic injection mold depend fundamentally on material selection and heat treatment precision. Depending on resin characteristics—such as glass fiber filling, flame retardants, or aggressive outgassing—our engineers select pre-hardened or fully hardened stainless tool steels optimized for wear resistance and thermal conductivity.
| Steel Grade | Standard Hardness | Corrosion / Wear Resistance | Optimal Resin Application | SPI Mold Class |
|---|---|---|---|---|
| ASSAB S136 / ESR | 48 - 54 HRC | Superior Corrosion & Polishability | Medical Grade PC, Optical Lenses, Clear Acrylic | Class 101 (1M+ Shots) |
| AISI H13 / Premium | 46 - 52 HRC | High Thermal Fatigue Resistance | Engineering Polymers (PA66+30%GF, PBT, PPS) | Class 101 / 102 |
| NAK80 (Pre-hardened) | 37 - 43 HRC | High Machinability & Uniform Structure | Consumer Electronics Housings, ABS, PP, POM | Class 102 / 103 |
| AMPCO 940 / Copper Alloy | 28 - 32 HRC | Ultra-High Thermal Conductivity | Conformal Cooling Inserts & Hot Spot Core Pins | Specialized Inserts |
Furthermore, the integration of 3D-printed metal Conformal Cooling Channels has revolutionized cycle time optimization. Traditional straight-drilled cooling lines leave hot spots in deep cavities, extending cooling times and inducing internal stresses. By deploying direct metal laser sintering (DMLS) to build curved cooling networks that follow the exact geometric contour of the part, cooling cycle times are reduced by up to 35% while eliminating part warpage.
Key Trends Shaping Plastic Tooling & Polymer Sourcing
Understanding the technological macro-shifts driving procurement decisions for tier-1 OEMs and enterprise buyers worldwide.
Smart Molds & Embedded Sensor IoT
Modern high-cavitation production molds are increasingly equipped with cavity pressure transducers, dynamic melt temperature sensors, and shot-counter microchips. Real-time telemetry allows automated injection parameter adjustments, preventing short shots and flash before defective parts are produced.
Metal-to-Plastic Conversion Engineering
Global procurement teams in automotive and aerospace are replacing heavy die-cast metal components with high-temperature engineering thermoplastics (PEEK, PEI, PPS, and PA66-GF50). Precision plastic mold design is critical to handling extreme resin shrinkage while maintaining structural rigidity and thermal stability.
Sustainable Bio-Resins & PCR Compliance
With global ESG mandates, factories must adapt mold designs for Post-Consumer Recycled (PCR) plastics and biodegradable resins. Because recycled materials exhibit variable melt flow indexes (MFI), our molds incorporate wider gate controls, optimized runner balancing, and precise venting design.
End-to-End Manufacturing Solutions Across Key Sectors
Deep expertise in design-for-manufacturability (DFM), cross-disciplinary hardware integration, and multi-cavity tooling execution.
Automotive Electronics & High-Voltage Connectors
Automotive electrical architectures demand strict insulation standards and vibration endurance. Our white PBT automotive connector molds feature sub-micron core pin alignment, ensuring micro-pitch pin channels remain flash-free. Insert molding techniques allow pre-stamped brass terminals to be encapsulated seamlessly during the molding phase.
Industrial Robotics & Mechatronics Housings
Robotic joint housings require high strength-to-weight ratios and precise bearing seat concentricity. Sunmy Hardware integrates custom 5-axis CNC post-machining with high-precision aluminum and plastic injection molding to achieve ±0.005 mm tolerances on bearing bores, minimizing backlash in servo-actuator assemblies.
Thermal Management & Power Electronics
Modern AI hardware, high-power LED arrays, and battery energy storage systems generate intense thermal loads. We design hybrid structural solutions combining skived-fin copper heatsinks, flexible laminated copper busbars, and over-molded flame-retardant enclosures (UL94-V0) to optimize heat dissipation and electrical isolation.
Semiconductor & Cleanroom Component Handling
For semiconductor wafer processing and critical fluid handling, high-purity polymers such as PTFE, PFA, and PEEK are required. Our machining and compression tooling facilities manufacture cleanroom-compatible gaskets, wafer carriers, and knurled gas-sealing connectors resistant to aggressive chemical attack and elevated temperatures.
Strict Quality Control & Intellectual Property Protection
How Sunmy Hardware delivers traceable quality documentation, secure data transfer, and seamless international shipping logistics.
Complete IP & Drawing Security
We enforce strict Non-Disclosure Agreements (NDAs) prior to receiving 2D/3D CAD files. All customer drawings (STEP, IGES, DXF) are encrypted and limited exclusively to authorized toolmakers and quality engineers.
CMM Dimensional Inspection
Every production mold and sample lot undergoes full 3D Coordinate Measuring Machine (CMM) analysis, optical profiling, and material certification (spectrometer verification). First Article Inspection (FAI) reports accompany every initial sample shipment.
DDP Export Logistics & Support
We manage customs clearance, export documentation, tariff classification, and Door-to-Door (DDP/DAP) sea, air, and express shipping to Europe, North America, Australia, and East Asia, eliminating supply chain friction for buyers.
Technology Roadmap & Future Tooling Vision (2025 - 2030)
Investing in automation, additive tooling manufacturing, and AI-assisted design algorithms to lead the next decade of plastic mold fabrication.
AI Automated DFM & Quoting
Deploying machine learning algorithms that instantly analyze 3D CAD geometries for draft angles, thin wall warnings, undercut collisions, and instant cost modeling, cutting RFQ turnaround time to under 4 hours.
Multi-Component Co-Injection Molds
Expanding advanced 2K/3K multi-shot rotary table molds and liquid silicone rubber (LSR) overmolding cells to eliminate secondary assembly steps for automotive controls and medical devices.
Zero-Carbon Tooling Infrastructure
Transitioning energy-intensive electric injection machines and CNC machining centers to 100% solar-assisted power, utilizing bio-degradable flushing fluids, and implementing closed-loop aluminum and steel scrap recycling.
Plastic Mold Design & Custom Manufacturing FAQ
Technical and procurement guidance addressing common inquiries from OEM buyers, project engineers, and global sourcing agents.
What design tolerances can Sunmy Hardware achieve for custom plastic injection molds?
For high-precision plastic components, our standard mold tooling tolerance is ±0.01 mm, while critical core/cavity features can hold tolerances down to ±0.005 mm through slow-wire EDM and mirror EDM machining. Final plastic part tolerances depend on resin shrinkage properties (e.g., Unfilled ABS can maintain ±0.02 mm, whereas high-shrinkage materials like PP or 30% Glass-Filled PA66 typically maintain ±0.05 mm to ±0.1 mm).
How does Sunmy Hardware handle DFM (Design for Manufacturability) analysis?
Every engineering drawing or 3D STEP file submitted to Sunmy Hardware undergoes a rigorous 24-hour DFM audit. Our engineers analyze wall thickness uniformity, draft angle sufficiency (minimum 1° to 2° suggested), gate position to hide cosmetic vestige, wall transition radii to prevent stress concentrations, ejector pin locations, and Moldflow fill/pack simulations.
Which SPI Mold Classes do you build, and what is your typical mold life warranty?
We design and build according to SPI (Society of the Plastics Industry) classifications:
- SPI Class 101: 1,000,000+ cycles. High-production tooling using hardened steel (S136, H13) with fully guided ejection and hardened slides.
- SPI Class 102: Up to 100,000 to 1,000,000 cycles. Medium to high production using steel grades like NAK80 or 718H.
- SPI Class 103: Up to 100,000 cycles. Low-volume prototype and bridge tooling utilizing P20 or pre-hardened steel.
What is your typical turnaround lead time from 3D design to T1 sample delivery?
For standard custom injection molds, the prototype tool build time takes approximately 15 to 25 calendar days. Complex, high-cavitation, or multi-slider hot runner production molds require 30 to 45 days. Rapid CNC machined prototypes or 3D printed samples can be dispatched within 3 to 5 business days for immediate design validation.
How do you protect customer Intellectual Property (IP) and proprietary CAD files?
IP security is a cornerstone of our business. We sign legally binding Non-Disclosure Agreements (NDAs) before reviewing any client drawings. As a direct factory with integrated CNC and tooling shops in Shenzhen, your CAD data stays strictly in-house and is never brokered to third-party traders.
Can you manufacture metal components and electrical busbars alongside plastic molding?
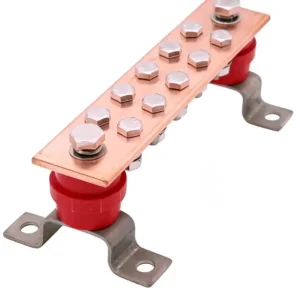
Yes. Sunmy Hardware is a true multi-process OEM manufacturer. We specialize in cross-disciplinary projects that combine precision CNC milling/turning, sheet metal stamping, copper busbars (flexible laminated & rigid grounding bars), die-casting, and plastic injection molding under one unified quality management system (QMS).
Precision Metal, Electrical & Thermal Hardware
Browse our additional line of custom fabricated copper busbars, die-cast housings, turned fittings, and semiconductor carriers.




Request a Comprehensive DFM Analysis & RFQ Quote
Send us your 3D CAD files (STEP, IGES, STL) or 2D dimensioned drawings. Our application engineering team will provide a thorough manufacturability evaluation, tool flow analysis, and competitive direct-factory quote within 24 hours.