
Precision Engineered Assemblies & Tooling Solutions
Explore our flagship OEM/ODM manufactured components, engineered with sub-tenth tolerances, CMM verification, and certified alloy metallurgy.

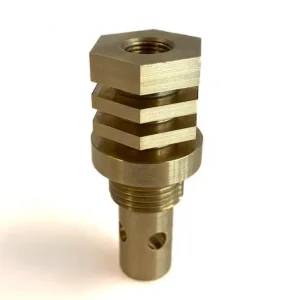





State of the Art: Technical Architecture of Modern Custom Precision Casting
In high-stakes industrial manufacturing, custom precision casting serves as the bedrock for near-net-shape component manufacturing. Unlike conventional sand casting which exhibits high dimensional variance and porous internal grain structures, advanced investment casting (lost-wax process), high-pressure die casting (HPDC), and vacuum-assisted shell molding deliver near-zero internal defects with exceptional surface finishes (Ra 1.6 to Ra 3.2 μm as-cast).
Modern global enterprises require a hybrid manufacturing workflow. The casting process establishes complex internal passages, thin-walled geometries, and weight-optimized hollow sections that are impossible to machine from solid billet stock without astronomical material waste. Subsequently, 5-axis CNC machining, wire EDM, and micro-honing operations finalize critical mating surfaces, thread channels, and bearing bores to tolerances as tight as ±0.005 mm.
Transitioning a component from full-billet CNC milling to investment casting combined with CNC finish-machining typically achieves a 35% to 60% reduction in total unit cost for production runs exceeding 500 units, while simultaneously reducing internal mechanical stress concentration.
Comparative Engineering Analysis: Casting Methodologies
| Casting Methodology | Primary Alloy Compatibility | Dimensional Tolerance (ISO 8062) | Surface Roughness (Ra) | Ideal Application Profile |
|---|---|---|---|---|
| Silica Sol Investment Casting | SS316L, 17-4PH, Inconel, Carbon Steel | CT4 - CT6 | Ra 1.6 - 3.2 μm | Complex thin-wall valves, impellers, medical tools |
| High-Pressure Die Casting (HPDC) | Aluminum (A380, ADC12), Zinc (Zamak) | CT5 - CT7 | Ra 0.8 - 1.6 μm | High-volume automotive brackets, electronics housings |
| Water Glass Investment Casting | Ductile Iron, Alloy Steel, Carbon Steel | CT7 - CT9 | Ra 6.3 - 12.5 μm | Heavy machinery links, agricultural structural parts |
| Vacuum-Assisted Precision Casting | Titanium Ti-6Al-4V, Cobalt-Chrome | CT4 - CT5 | Ra 1.6 - 3.2 μm | Aerospace engine vanes, surgical implants |
The Strategic Advantages of China's Precision Casting Ecosystem
How localized industrial clusters in Shenzhen and the Pearl River Delta deliver unmatched speed, cost control, and technical rigor for global supply chains.
Full Vertical Integration
China’s premier casting hubs combine mold making, alloy smelting, precision investment casting, multi-axis machining, heat treatment (T6, Annealing, Passivation), and surface finishing under a single unified Quality Management System (QMS).
Accelerated Prototype-to-Scale
Using 3D printed wax models (SLA/SLS) and rapid tooling aluminum dies, prototype samples are produced in as few as 7–10 working days, allowing OEM engineering teams to execute physical test loops before committing to hard tooling.
Rigorous Traceability & QA
Leading Chinese casting facilities operate ISO 9001 and IATF 16949 certified quality systems. Shipments include complete spectrographic chemical analysis, tensile test certificates, CMM dimensional evaluation, and non-destructive X-ray testing.
Industry Trends: AI, Simulation & Sustainable Metallurgy
How smart manufacturing technologies are revolutionizing metal casting accuracy and eliminating systemic defects.
ProCAST & Finite Element Simulation
Before cutting steel for molds, digital thermal and mold-filling simulation models melt flow, solidification fronts, and shrinkage stress zones. This eliminates micro-porosity, cold shuts, and gas inclusions early in DFM engineering.
Closed-Loop Automated Quality Control
Integration of automated optical inspection (AOI) scanners and 3D laser-CMM arm systems directly on the foundry floor provides real-time feedback, enabling automated adjustments to pouring temperatures and pressure curves.
Green Metallurgy & Low-Carbon Alloys
Factories are shifting to electric induction furnaces powered by clean grids, achieving up to 98% metal recycling rates and complying with European Union Carbon Border Adjustment Mechanism (CBAM) requirements.
Cross-Industry Application Scenarios
From mission-critical medical enclosures to high-stress robotic joints, precision casting delivers uncompromising strength and geometric complexity.
Medical & Diagnostic Housings
Material: SS316L / High-Transparency Optical PC
Key Need: Biocompatibility, hermetic sealing, chemical resistance against sterilisers.
Solution: Deep-drawn and investment cast housings with electro-polished surface finish (Ra < 0.4 μm).
Robotics & Motion Control
Material: 7075 Aluminum / ADC12
Key Need: High strength-to-weight ratio, zero backlash bearing fits.
Solution: 5-axis CNC post-machined die-cast robot finger joints and swivel arms with tight runout tolerances.
Industrial Fluid & Thermal Systems
Material: C36000 Brass / Aluminum 6061
Key Need: High thermal conductivity, leak-free internal cooling passages.
Solution: Investment cast water valve bodies and multi-channel liquid cooling blocks certified for high-pressure operation.
Global Procurement Guide: Mitigating Technical & Supply Chain Risk
When sourcing custom metal casting and precision machined assemblies internationally, global enterprise buyers must evaluate suppliers across four vital criteria beyond basic price-per-piece:
Precision Casting Technical Q&A
Detailed answers to technical queries encountered by engineering and procurement teams.
Standard investment casting tooling typically takes 15 to 20 business days. For rapid prototype verification, SLA 3D printed wax models can deliver initial cast metal samples within 7 to 10 days. High-pressure die casting dies usually require 25 to 35 days depending on mold complexity and slider mechanisms.
Porosity control is managed through a multi-tier approach: 1) ProCAST numerical mold flow simulation to optimize gate geometry and riser positions; 2) Vacuum-assisted casting technology; and 3) 100% industrial X-ray non-destructive testing (NDT) combined with hydrostatic pressure testing for fluid-carrying components.
As-cast investment components achieve ISO 8062 CT4–CT6 dimensional tolerance (approx. ±0.1mm to ±0.3mm depending on part envelope). Precision features such as bearing journals, O-ring seal grooves, and threaded mounting holes are post-machined on CNC centers to achieve ±0.005mm tolerances.
Yes. Our foundry facilities are equipped with medium-frequency vacuum induction melting furnaces capable of pouring SS304, SS316L, 17-4PH precipitation hardening stainless steel, Duplex 2205, Hastelloy, and Cobalt-Chromium alloys with complete chemical spectrum analysis certification.
Custom OEM Metal & Polymer Assemblies
Explore further custom hardware products manufactured to customer drawings and international engineering standards.






Accelerate Your Hardware Development Program
Submit your 3D CAD files (STEP, IGES, X_T) or 2D technical drawings today. Our senior metallurgical and machining engineers will provide a comprehensive DFM analysis and quotation within 24 hours.