
OEM/ODM Custom Hardware & Polymer Components
Explore our top-tier precision turned parts, castings, and engineered plastic components designed for global tier-1 supply chains.
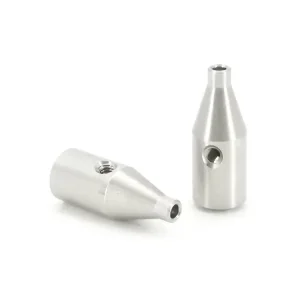
ODM Custom CNC Turned Aluminum Nozzle & Adapter Bodies Manufacturers
View Product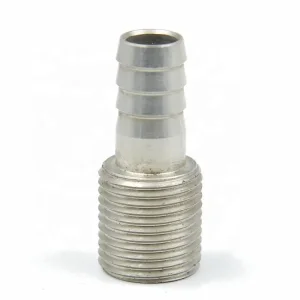
China Custom CNC Turned Hose Barb Fittings & Threaded Adapters
View Product
Custom Stainless Steel Mounting Bracket Factories
View Product
OEM Premium Custom Stainless Steel Casting Services
View Product
China Precision Capillary Stainless Steel Pipe & Tube
View Product
OEM Aluminum Die-Cast Transmission Housing
View Product
OEM Precision Injection Molded POM Plastic Gears
View Product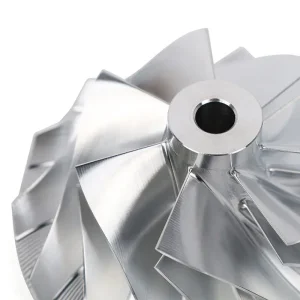
OEM Custom 5-Axis CNC Machined Billet Aluminum Impeller
View Product1. The Paradigm Shift to Precision Polymer Gearing in Global OEM Manufacturing
Analyzing global economic forces, weight reduction mandates, NVH damping standards, and the total cost of ownership (TCO) advantage offered by Chinese precision gear exporters.
Metal-to-Plastic Conversion
Global Tier-1 manufacturers in automotive, robotics, and medical devices are systematically replacing traditional brass and steel gearing with advanced engineering polymers. The conversion yields an average 68% weight reduction, lowers rotational inertia, and eliminates external lubrication dependencies.
Acoustic & NVH Suppression
Noise, Vibration, and Harshness (NVH) compliance has become a core KPI for smart home systems, EV actuators, and surgical tools. High-precision polymer gears exhibit superior internal viscoelastic damping, attenuating gear mesh noise by up to 12 dB(A) compared to metallic kinematic trains.
Total Cost of Ownership (TCO)
While metal gearing requires complex multi-step hobbing, deburring, heat treatment, and grinding, multi-cavity injection molding produces net-shape precision gears in single-second cycle times, achieving scalable cost drops exceeding 75% at volume.
2. Kinematic Engineering, Polymer Tribology & Tooling Architecture
Precision plastic gear design requires rigorous mathematical modeling of non-uniform material shrinkage, orientation-dependent anisotropy, thermal expansion offset, and involute tooth profile modifications.
1. Shrinkage & Distortion Compensation
Polymer crystallographic contraction during mold cooling creates volumetric shrinkage ranging from 1.5% to 3.0% (e.g., Unfilled POM). Sunmy Hardware utilizes proprietary mold cavity modification matrices, adjusting the involute profile using FEA and Moldflow warpage analysis to achieve true involute accuracy post-cooling.
2. Tribological Material Engineering
Selection of resin systems directly governs wear resistance, coefficient of friction (CoF), and PV (pressure-velocity) limits. We formulate custom compounds integrating internal lubricants such as PTFE (5-15%), Silicone oil, or Molybdenum Disulfide (MoS2) into PA66, PEEK, or POM matrix polymers.
3. Concentricity & Weld-Line Positioning
Multi-gate pin-point or diaphragm gating structures are dynamically balanced to eliminate weld lines at the gear tooth root. This guarantees uniform radial fiber alignment in glass-reinforced resins, mitigating premature fatigue fractures across high-load tooth flanks.
Polymer Gear Material Selection & Performance Specification
| Polymer Base Grade | Filler / Modifier | Tensile Strength (MPa) | Flexural Modulus (GPa) | Continuous Temp (°C) | Primary Industrial Use Case |
|---|---|---|---|---|---|
| POM-C (Polyacetal Copolymer) | Unfilled / 10% PTFE | 65 - 70 | 2.8 - 3.2 | -40 to 105 | High-precision consumer electronics, spur/helical gears, meters. |
| PA66 (Polyamide 66) | 30% Glass Fiber (GF30) | 175 - 190 | 8.5 - 9.5 | -30 to 135 | Automotive under-hood actuators, high-torque transmission drives. |
| PBT (Polybutylene Terephthalate) | 15% Mineral + PTFE | 85 - 95 | 4.2 - 5.0 | -40 to 120 | Dimensionally stable water meter gears, low moisture absorption. |
| PEEK (Polyetheretherketone) | 30% Carbon Fiber / PTFE | 210 - 240 | 18.0 - 22.0 | -50 to 250 | Aerospace actuators, surgical robotics, severe chemical environments. |
| PPS (Polyphenylene Sulfide) | 40% Glass Fiber | 150 - 165 | 12.5 - 14.0 | -40 to 200 | High-heat fluid pumps, automotive throttle valve control gears. |
3. Tooling Precision, DIN 3962 Metrology & Quality Control
Sub-micron cavity erosion, active mold temperature zoning, and dedicated CNC gear measurement centers ensure repeat compliance to international gearing standards.
High-Speed EDM Wire Cut
Tooling cavities are machined via Swiss-made Makino high-speed wire EDM and micro-spark erosion, executing tooth profiles with an electrode contour tolerance down to ±0.0015 mm.
Conformal Cooling Channels
3D-printed metal conformal cooling channels within core pins ensure perfectly isotropic thermal extraction, mitigating gear dish distortion and pitch ovality during rapid cycling.
DIN 3962 Class 7 Metrology
Inspected on Osaka or Zeiss CNC Gear Inspection Centers. Comprehensive inspection reports include total cumulative pitch error ($F_p$), single pitch error ($f_p$), and tooth profile discrepancy ($f_f$).
100% In-Line Cavity Pressure
Piezoelectric cavity pressure sensors (Kistler) continuously monitor melt packing in real-time, automatically segregating any short-shot or flash-affected parts at the robot arm end-effector.
4. Specialized Industry Deployments & Kinematic Assemblies
Custom plastic gear solutions engineered to meet rigorous performance thresholds across demanding global vertical sectors.
Automotive Powertrain & Actuators
Used in electronic throttle control (ETC), electronic parking brakes (EPB), HVAC damper drives, and side-mirror folding mechanisms. Utilizes heat-stabilized PA66-GF30 and PEEK compounds to withstand under-hood ambient spikes up to 150°C under severe vibration.
Medical Devices & Surgical Robotics
Integrated into peristaltic infusion pumps, automated insulin delivery pens, and robotic joint gearboxes. Fabricated under ISO 13485 cleanroom protocols using USP Class VI biocompatible POM and PEEK resins ensuring zero outgassing and smooth micro-stepping.
Smart Home Robotics & Appliances
High-torque planetary gearheads for robotic vacuum wheel drives, motorized window blinds, and smart door locks. Designed for ultra-quiet acoustic operation (<35 dB), high shock-load tolerance, and operational lifespan exceeding 500,000 continuous drive cycles.
5. Global Export Compliance, IP Safeguards & Supply Chain Risk Management
Sunmy Hardware operates as an audited export-oriented manufacturer, protecting buyer intellectual property while facilitating seamless customs clearance across European, North American, and Asian markets.
Bilateral non-disclosure agreements executed prior to CAD exchange. Encrypted internal server storage ensures strict data compartmentalization.
In-depth DFM report provided within 24 hours. Gate location, draft angles, wall thickness uniformity, and filling speed optimized up front.
First-article inspection (FAI) report accompanied by raw material mill certificates, RoHS, REACH, and CMM dimension verification data.
Statistical Process Control (SPC) deployed throughout production. Continuous tracking of Cpk values (>1.33) on key pitch diameters.
Vacuum-sealed anti-static packaging with desiccants. Flexible logistics delivery including DDP, FOB Shenzhen, CIF, or air express shipment.
Plastic Gear Tooling & Manufacturing Engineering FAQ
Direct answers to critical procurement and engineering queries regarding tolerances, material selection, mold life, and export terms.
How do you guarantee AGMA Class 10 / DIN Class 7 accuracy in multi-cavity injection molds?
Achieving high DIN/AGMA gear accuracy relies on three core factors: (1) Utilizing Swiss wire-EDM to cut core/cavity inserts with sub-2 micron tool precision; (2) Applying Moldflow shrinkage-compensation geometry directly to the 3D CAD model before cavity cutting; and (3) Controlling thermal balance via independent mold temperature control loops per cavity. Every production lot is verified on our Osaka CNC Gear Measuring Center.
What polymer material is best for high-torque plastic gear applications?
For moderate temperature high-torque drives, PA66 reinforced with 30% glass fiber (PA66-GF30) offers outstanding tensile strength (up to 190 MPa). For extreme thermal or chemical environments (up to 250°C continuous), carbon-fiber filled PEEK (PEEK-CF30) is specified. When minimal friction and moisture stability are required, POM-C modified with PTFE internal lubricants is preferred.
How does Sunmy Hardware handle weld-line weakening at gear tooth roots?
Weld lines occurring at a gear tooth root reduce fatigue strength by up to 50%. We mitigate this by using multi-point diaphragm or submarine gating engineered via Moldflow simulation to push melt-front convergence into non-critical web areas rather than the tooth root, maintaining 95%+ matrix strength across all load-bearing teeth.
What is the standard tooling lead time and expected mold life for custom plastic gear molds?
Standard steel gear mold lead time is 25 to 35 calendar days from final DFM approval to T1 sample delivery. Molds constructed with hardened ASSAB S136 or NAK80 tool steels (52-54 HRC) are guaranteed for 1,000,000 shots under standard maintenance schedules.
Do you support prototype gear sampling prior to committing to production tooling?
Yes. We provide rapid prototyping options including 5-axis CNC machining of engineering plastic billets (POM, PEEK, PA66), high-resolution SLA/SLS 3D printing, and rapid soft-tooling (aluminum molds) to evaluate kinematic mesh performance before cutting production multi-cavity steel molds.
Custom Machined & Molded Engineering Components
Review our comprehensive catalog of high-precision connectors, custom electronic enclosures, and complex mechanical hardware exported globally.

ODM Custom Aluminum Electronic Enclosure Suppliers
View Product
High-Quality Custom Flexible Laminated Copper Busbar
View Product
ODM High-Precision Gold-Plated Brass Pogo Pins for PCB
View Product
China Precision Knurled Brass Threaded Connector Supplier
View Product
Automotive Transmission Retarder Engine Clutch Oil Pan
View Product
8-Inch CNC Machined Aluminum Semiconductor Wafer Carrier
View Product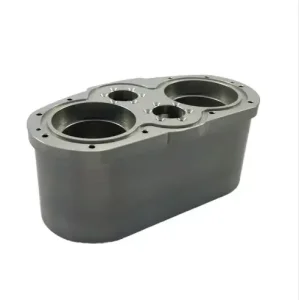
5-Axis CNC Steel Universal Joint Base & Gearbox Shell
View Product