
Precision OEM & Custom Hardware Solutions
Explore our featured core tooling, high-precision metal stamping, die casting, and specialized turned components engineered for seamless integration into complex hot runner systems and automation machinery.







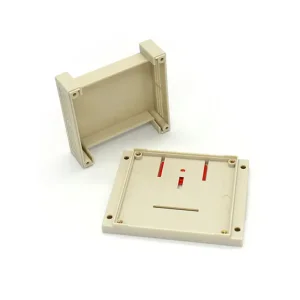
The Paradigm Shift in Polymer Processing: Next-Generation Hot Runner Mold Engineering
In high-volume polymer manufacturing, the transition from conventional cold runner tooling to fully integrated Hot Runner Mold Systems represents the single largest leap in thermodynamic optimization, material yield enhancement, and operational cost containment over the last two decades.
As global consumer electronics, medical diagnostics, packaging, and automotive industries demand ultra-thin walls, flawless optical aesthetics, and zero-defect zero-scrap production parameters, hot runner mold technology has evolved from a simple heated runner block into a multi-zone, sensor-driven micro-thermodynamic control center.
At Sunmy Hardware, our engineering division combines deep metallurgy expertise, 5-axis CNC sub-micron machining, advanced rheological Moldflow simulations, and proprietary manifold heating technology to deliver hot runner tooling that consistently yields sub-second cycle time reductions, zero gate vestige, and unprecedented thermal stability across multi-cavity architectures.
Global Procurement Strategy: Evaluating Hot Runner Mold Suppliers Beyond Initial Tooling CAPEX
Enterprise procurement officers and tooling engineers are shifting their evaluation metrics from upfront mold acquisition cost to total cost of ownership (TCO) and operational resilience.
Thermal Uniformity & Rheology
Uneven heat distribution leads to degradation of temperature-sensitive polymers (e.g., PEEK, PC, PET-G), non-uniform cavity fill, warpage, and weld line weakness. Modern buyers require documented manifold temperature stability within ±1.0°C across all drop locations.
Sequential Valve Gate Control
For large structural components like automotive bumpers or optical instrument enclosures, pneumatic or servo-electric sequential valve gating (SVG) eliminates sink marks and weld lines by controlling melt front convergence in real-time.
Component Interchangeability
Global manufacturing plants cannot afford extended downtime. Procurement demands standardized, high-wear interchangeable components—such as titanium-coated nozzle tips, ceramic insulators, and drop-in tubular heaters.
| System Architecture Parameter | Cold Runner Molds | Standard Hot Runner Molds | Sunmy Precision Valve-Gate Hot Runner Molds |
|---|---|---|---|
| Raw Material Utilization | 70% – 85% (Scrap generated per cycle) | 98% – 99% (No runner sprue scrap) | 99.9% (Zero runner, zero flash, zero gate waste) |
| Cycle Time Efficiency | Base Reference (Cooling runner takes time) | 15% – 25% Faster | 35% – 50% Faster (Direct part cavity cooling focus) |
| Gate Cosmetic Quality | Requires secondary trimming / sprue mark | Small pin mark / thermal vestige | Class-A Flush Surface (Servo Valve Pin Cutoff) |
| Resin Thermal Degradation Risk | Low | Moderate (If dead spots exist in manifold) | Zero (Polished flow channels, optimized radius elbows) |
| Tooling Service Life (Cycles) | 500,000 – 1,000,000 | 1,000,000 – 3,000,000 | 5,000,000+ Guaranteed (Premium H13/S136 Hardened Steel) |
Global Industry Trends Transforming Hot Runner Tooling
As smart manufacturing matures, hot runner system design is transitioning from static mechanical tooling into intelligent, self-regulating cyber-physical injection platforms.
1. Additive Manufacturing & Conformal Cooling Inserts
3D printing tool steel via Direct Metal Laser Sintering (DMLS) allows Sunmy engineers to create internal conformal cooling channels that closely follow the 3D contour of complex core and cavity inserts. Combined with hot runner direct drop nozzles, heat is extracted uniformly, drastically reducing cycle times and eliminating localized warpage in thin-wall medical devices and electronic housings.
2. Smart Closed-Loop IoT Thermal & Pressure Sensors
Modern high-cavitation molds (e.g., 64-cavity or 128-cavity medical syringe tools) integrate piezoelectric dynamic cavity pressure sensors and real-time thermocouple feedback at every single nozzle tip. The system automatically adjusts individual heater zone power outputs in micro-seconds to compensate for ambient thermal shifts or resin viscosity fluctuations.
3. Processing Bio-Resins & PCR Recycled Polymers
Post-consumer recycled (PCR) plastics and biodegradable polymers (like PLA or PHA) possess narrow thermal processing windows and higher sensitivity to shear-induced thermal degradation. Sunmy's advanced hot runner manifolds feature flow channels designed via Computational Fluid Dynamics (CFD) to deliver smooth shear transitions and prevent melt breakdown during high-speed injection.
4. Servo-Electric Actuation over Pneumatics
Cleanroom manufacturing environments (ISO Class 7 and Class 8) are phasing out traditional pneumatic valve gate actuators due to risk of oil-mist contamination and compressed air energy loss. All-electric servo-driven valve gate plates provide sub-micron position control, variable opening speed profiles, and 100% cleanroom compliance.
Supply Chain Resilience & Engineering Agility at Sunmy Hardware
Located in Shenzhen, the heart of China’s advanced precision manufacturing corridor, Shenzhen Sunmy Hardware Co., Ltd. leverages a highly concentrated industrial ecosystem. We bridge world-class mold design engineering with direct factory floor speed and control.
Vertical Integration Under One Roof
From 5-axis CNC mold base milling, wire EDM core cutting, and Swiss precision turned valve pins to final CMM inspection, Sunmy maintains full internal quality sovereignty.
24-Hour DFM & Fast T1 Sample Delivery
Our engineering team delivers complete Moldflow filling reports and Design for Manufacturability (DFM) analysis within 24 hours of CAD submission, achieving initial T1 sample trials in as fast as 21 days.
IP Protection & Strict Quality Protocols
We protect global client IP through enforceable NDA agreements and execute complete First Article Inspection (FAI) reports, mill test material certificates, and CMM dimension verification before export.
Sunmy Tooling Specifications Summary
- Mold Base Steel LKM, P20, S50C, HASCO Standard
- Core & Cavity Steel ASSAB S136, H13, NAK80, 1.2344
- Hot Runner Brands Yudo, Mold-Masters, Synventive, Husky, Custom
- Gating Options Valve Gate, Thermal Tip, Edge Gate, Direct Sprue
- Machining Precision ±0.005 mm (CMM Verified)
- Certifications ISO 9001:2015, RoHS Compliant
Target Industry Deployment & Specific Tooling Scenarios
Hot runner system requirements vary radically across sectors. Here is how Sunmy Hardware engineers specialized tooling for diverse global applications.
Automotive Exterior & Optics
Scenarios: Headlamp optical light guides (PMMA/PC), door panels, front grilles, radiator support mounts.
Tooling Strategy: Multi-drop sequential pneumatic/electric valve gate systems preventing weld lines across long flow ratios and guaranteeing optical clarity.
Medical & Micro-Fluidics
Scenarios: Syringe barrels, blood diagnostic cassettes, IV connectors, sterile pipette tips.
Tooling Strategy: Ultra-high cavitation (32 to 128 cavities) hot runner systems built with medical-grade S136 stainless steel, mirror polished to Ra 0.05 μm with zero flash.
Consumer Electronics & Smart Devices
Scenarios: Thin-wall smartphone frames, TWS earbud cases, VR headset structural brackets.
Tooling Strategy: Compact hot runner nozzles allowing tight gate center-to-center distances, optimized for glass-filled engineering plastics (PA66+30%GF, PC+ABS).
Frequently Asked Questions by Hot Runner Procurement & Tooling Engineers
Get expert insights into hot runner mold design, maintenance protocols, resin selection, and global tooling logistics.
What is the difference between a Thermal Tip Gate and a Valve Gate Hot Runner System?
A Thermal Tip System uses a continuously heated tip at the gate location. As the mold opens, the plastic at the gate freezes self-consistently due to mold cooling, leaving a small vestige or nub on the part. It is cost-effective and ideal for standard parts where aesthetic gate perfection is not critical.
A Valve Gate System uses a mechanically driven steel pin (pneumatic, hydraulic, or servo-electric) that physically moves forward to seal the gate flush with the cavity wall before the mold opens. This leaves virtually zero gate vestige, eliminates stringing/drooling, permits larger gate diameters for faster filling, and allows sequential opening control for large parts.
How does Sunmy Hardware ensure accurate thermal balance across high-cavity manifolds?
We achieve thermal uniformity through a three-stage design and testing protocol:
- FEA Thermal Simulation: Finite Element Analysis is conducted on the 3D manifold to place heater elements and determine power density distribution.
- Natural Rheology Balancing: Melt flow channels feature identical flow lengths, diameters, and smooth turn radii to ensure equal pressure drop and shear heating to all drops.
- Multi-Zone Independent Control: Every drop tip and manifold section has dedicated thermocouples and closed-loop PID controller feedback, keeping temperature deltas within ±1.0°C.
Which tool steels are recommended for processing corrosive or abrasive polymers?
For abrasive materials (such as glass-fiber filled Polyamide or PBT), we utilize H13 or 1.2344 steel hardened to HRC 52-54, with Titanium Nitride (TiN) or PVD coatings on nozzle tips and valve pins. For corrosive polymers (like PVC or flame-retardant resins emitting acidic gas), we specify ASSAB S136 or 1.2083 stainless steel hardened to HRC 48-52, providing exceptional rust and chemical corrosion resistance.
How do you prevent color-change contamination in hot runner flow channels?
Color change speed depends heavily on manifold internal surface finish and channel geometry. Sunmy designs manifolds with zero "dead spots" or sharp corners where stagnant resin can trap. Flow channels are gun-drilled and mechanically polished to a mirror finish. Optional ceramic coatings can also be applied to reduce polymer adhesion during color purges.
What lead time can buyers expect for custom hot runner molds from Sunmy Hardware?
Our standard manufacturing timelines are engineered for high-velocity project launches:
- DFM & Moldflow Report: Within 24 Hours.
- 3D Tooling Design Approval: 3 – 5 Days.
- Prototype / Low-Cavitation Tooling (T1 Samples): 21 – 28 Days.
- High-Cavitation Production Tooling: 35 – 45 Days.
How are spare parts and maintenance handled for international clients?
Every hot runner mold delivered by Sunmy comes with a complete digital engineering package and a critical maintenance kit. This includes spare heating bands, thermocouples, valve pins, seals, and nozzle tips. We utilize globally standardized threads and components (compatible with HASCO, DME, or MISUMI standards) so parts can also be sourced locally in Europe or North America if urgent replacements are required.
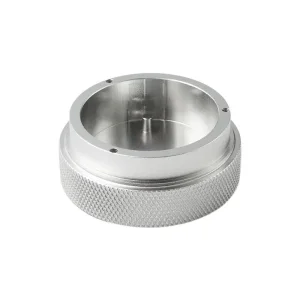
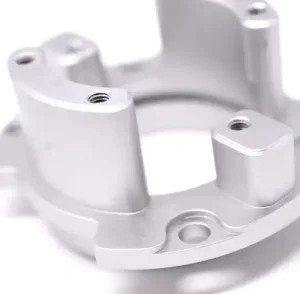
High-Precision Turned, Machined & Stamped OEM Parts
Discover our extended line of precision components manufactured with sub-micron CNC turning, 5-axis milling, and custom alloy stamping to complement your complete manufacturing system.





Ready to Optimize Your Polymer Tooling & Reduce Injection Cycle Times?
Upload your 3D CAD drawings (STEP, IGES, X_T) or physical product parameters. Our senior tooling directors will provide a complete Moldflow thermal balance report, DFM analysis, and factory-direct quote within 24 hours.
Request Free DFM & Hot Runner Quote