2026 Top Titanium Machining Types for Global Buyers

Time:2026-10-25 Author:Liam
0%

For global buyers, Titanium Machining is no longer a simple material-removal decision. In 2026, suppliers must balance geometry, alloy behavior, surface quality, delivery risk, and traceability. Titanium reacts strongly to heat. Poor tool paths can create built-up edges, chatter, or hidden surface damage. That damage may appear minor. It is not.

This guide examines the top titanium machining types used across aerospace, medical, energy, marine, and high-performance industrial applications. It considers CNC milling, turning, Swiss machining, five-axis cutting, drilling, grinding, and hybrid finishing. Each process has a practical place. None is universally best. A compact medical component may need Swiss machining, while a large aircraft fitting may demand five-axis milling. Experienced shops verify cutting data through controlled trials, not assumptions. They inspect tool wear, coolant flow, dimensional stability, and final surface condition. Buyers should request material certificates, inspection records, capability evidence, and realistic lead times. Claims deserve testing.

The discussion also recognizes an uncomfortable truth: published cycle times often exclude setup changes, rework, and inspection delays. This overview focuses on decisions that survive production, not attractive quotations alone. It explains how alloy grade, part shape, tolerance, batch size, and certification requirements influence process selection. Readers can compare methods with clearer expectations and fewer surprises. Still, no article can replace a qualified process review. Every critical part deserves validation. That is where reliability begins.
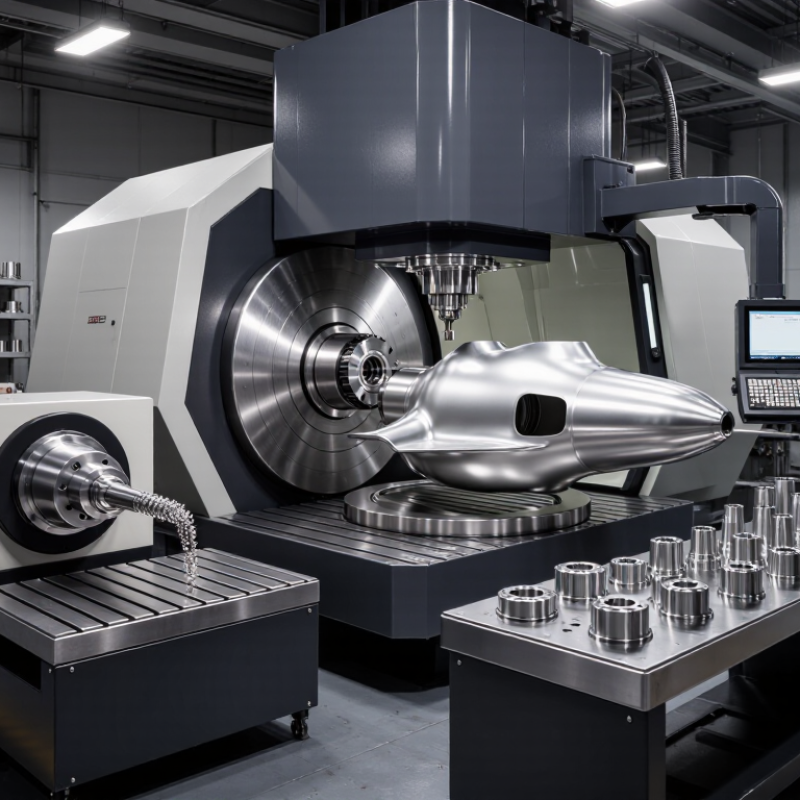
2026 Top Titanium Machining Types for Global Buyers

2026 Titanium Machining Scope: ~4.5 g/cm³ Density and 1,668°C Melting Point

2026 Top Titanium Machining Types for Global Buyers

Titanium combines a density of about 4.5 g/cm³ with a melting point near 1,668°C. These figures explain its value in aerospace, medical, energy, and high-performance equipment. The 2025 USGS Mineral Commodity Summaries identifies titanium sponge as a critical input for advanced alloy production. However, low density does not mean easy machining. Titanium retains heat near the cutting zone. Its elastic recovery can also cause vibration and dimensional drift.

CNC turning suits shafts, rings, and threaded components. CNC milling handles pockets, curved surfaces, and complex housings. Drilling requires sharp tools, stable clamping, and controlled chip evacuation. Grinding can improve surface finish, but excessive pressure may create heat damage. Electrical discharge machining works for difficult profiles when electrical conductivity and tolerances permit. According to ASM machining guidance, low cutting speeds and generous coolant flow often protect tool edges. Actual settings still depend on grade, geometry, and machine rigidity. A perfect parameter chart does not exist.

Tips: Ask for the titanium grade, density tolerance, melting-point reference, heat-treatment condition, and required surface finish. Request inspection records for hardness, dimensions, and burr control. Do not compare suppliers by cycle time alone. Titanium may look simple on a drawing, yet thin walls can distort after release. I have seen buyers overlook this risk. A small trial batch usually reveals more than a confident quotation.

Classify ASTM Grades: Grade 2, Grade 5 Ti-6Al-4V, and Grade 23

2026 Top Titanium Machining Types for Global Buyers

ASTM titanium grades strongly influence machining methods, tool life, and final component reliability. Grade 2 is commercially pure titanium with good corrosion resistance and moderate strength. It machines more easily than alloyed grades, making it suitable for covers, tubing parts, and chemical-processing components. Sharp carbide tools, steady coolant flow, and low cutting pressure help prevent heat buildup.

Grade 5, Ti-6Al-4V, offers higher strength and wider aerospace, medical, and industrial use. It resists deformation, but it also generates heat quickly during turning, milling, and drilling. Machinists usually choose rigid workholding, controlled feeds, and frequent tool inspection. A small dull edge can create discoloration, burrs, or an oversized hole.

Grade 23 is Ti-6Al-4V ELI, with reduced oxygen, nitrogen, and iron limits. Its improved ductility and fracture toughness support demanding medical and low-temperature applications. Buyers should request the exact ASTM specification, heat number, chemical analysis, and mechanical test records. Do not treat Grade 23 as simply cleaner Grade 5. That shortcut is convenient, but incomplete.

Machining type matters too. Deep pockets may require adaptive milling, while thin walls need reduced cutting forces and careful support. For drilled holes, chip evacuation deserves close attention. Small details matter. Global buyers should also verify dimensional reports, surface-finish data, packaging protection, and traceability before approving production. One overlooked document can delay an otherwise precise titanium order.

2026 Top Titanium Machining Types for Global Buyers - Classify ASTM Grades: Grade 2, Grade 5 Ti-6Al-4V, and Grade 23

Practical comparison of common titanium machining processes, ASTM grade characteristics, and purchasing considerations for international buyers

Machining Type Best-Suited ASTM Grade Typical Titanium Applications Key Grade Characteristics Machining Advantages Main Technical Challenges Recommended Production Controls Typical Buyer Requirements
CNC Turning
External diameters, internal bores, threads, shoulders, and rotational components
Grade 2
Commercially pure titanium
Suitable for corrosion-resistant rings, sleeves, shafts, and fittings

Grade 5
Ti-6Al-4V
Suitable for high-strength aerospace and industrial components
Valve parts, flanges, bushings, threaded connectors, medical instrument components, and aerospace fittings Grade 2 offers good corrosion resistance and moderate strength.

Grade 5 provides substantially higher strength than commercially pure grades, but generally requires more controlled cutting conditions.
Efficient for repeatable cylindrical parts; supports tight dimensional control when workholding, tool overhang, and thermal conditions are properly managed Low thermal conductivity concentrates heat near the cutting edge. Titanium can react with tools, work-harden under poor cutting conditions, and deflect during slender-part turning. Use rigid workholding, sharp positive-geometry carbide tooling, adequate coolant delivery, stable chip evacuation, and avoid dwelling in the cut. Confirm raw-material standard, bar or billet condition, thread specification, concentricity, runout, surface roughness, and inspection method before production.
CNC Milling
Slots, pockets, contours, steps, holes, and prismatic components
Grade 5
Ti-6Al-4V
Widely selected for structural parts and high-strength machined components

Grade 23
Ti-6Al-4V ELI
Selected where enhanced toughness, ductility, or medical-material requirements are important
Lightweight brackets, housings, orthopedic components, structural supports, manifolds, and complex custom parts Grade 5 combines low density with high strength and is an alpha-beta titanium alloy.

Grade 23 is an extra-low-interstitial version of Ti-6Al-4V, commonly used when improved fracture toughness and ductility are required.
Produces complex profiles and multi-face features; compatible with 3-axis, 4-axis, and 5-axis machining strategies Heat buildup, tool chipping, vibration, burr formation, and reduced tool life may occur if radial engagement, feed, or toolpath changes are poorly controlled. Prefer constant tool engagement, short tool overhang, high-pressure coolant where appropriate, smooth entry and exit moves, and conservative radial engagement. Request a fully dimensioned drawing, datum structure, material certificate, heat-treatment condition, geometric tolerances, and surface-finish limits.
5-Axis Simultaneous Milling
Complex freeform surfaces, angled features, and difficult-to-reach areas
Grade 5
Common choice for aerospace and high-strength components

Grade 23
Suitable for selected medical and performance-critical components
Turbine-related components, aerospace brackets, implantable components, complex housings, and contoured structural parts Grade 5 offers a high strength-to-weight ratio. Grade 23 retains the Ti-6Al-4V alloy family while lowering interstitial-element limits compared with standard Grade 5. Reduces setups, improves access to compound surfaces, and can maintain a more favorable tool-contact angle over complex geometry Simultaneous-axis motion can magnify tool deflection, surface waviness, chatter, and collision risk. Thin walls may distort during machining. Use verified CAM simulation, stable fixturing, controlled stock allowance, adaptive toolpaths, and finishing passes separated from heavy roughing. Define coordinate systems, datum transfer requirements, model-based inspection data, allowable blending, and inspection records for critical surfaces.
CNC Drilling and Reaming
Through-holes, blind holes, precision bores, and cross-drilled features
Grade 2
Frequently used for corrosion-resistant hardware

Grade 5 / Grade 23
Used for high-strength and medical-grade components
Bolt holes, oil passages, implant features, aircraft fittings, brackets, and precision alignment holes Titanium grades have low thermal conductivity, so heat removal and chip evacuation are important. Grade 5 and Grade 23 generally require more robust drilling control than Grade 2. Supports accurate hole production when drill geometry, coolant flow, peck strategy, and workpiece support are correctly selected Drill rubbing, work hardening, chip packing, hole oversize, burrs, and tool breakage can result from insufficient feed or poor chip evacuation. Maintain positive cutting action, use suitable point geometry, provide reliable coolant access, support thin sections, and inspect hole size and cylindricity. Specify hole diameter, tolerance class, positional tolerance, entry and exit burr limits, thread details, and whether deburring is permitted on functional edges.
Swiss-Type CNC Machining
Small-diameter, slender, and high-volume precision parts
Grade 2
Suitable for small corrosion-resistant precision parts

Grade 5
Suitable for stronger miniature components and medical hardware
Small pins, sleeves, bone screws, connectors, instrument parts, and miniature turned components Grade 2 is generally easier to cut than Grade 5 because of its lower strength. Grade 5 supports higher mechanical loads but places greater demands on tooling and process stability. Guide-bushing support limits deflection and enables efficient production of long, small-diameter components Small tools are vulnerable to heat, edge chipping, and chip entanglement. Slender components may still distort during cutoff or secondary operations. Use close tool projection, controlled chip breaking, reliable bar support, consistent material condition, and separate inspection for miniature features. Confirm minimum feature size, burr criteria, thread gaging, concentricity, cleanliness, packaging, and lot traceability requirements.
Grinding and Precision Finishing
Tight tolerances, controlled surface texture, and final sizing
Grade 2
Used for corrosion-resistant precision surfaces

Grade 5 / Grade 23
Used for high-strength or medical components requiring controlled finish
Sealing surfaces, bearing seats, implant interfaces, precision bores, and close-tolerance mating surfaces Titanium can generate heat during grinding. Grade 5 and Grade 23 require careful thermal control to avoid surface damage and dimensional variation. Can achieve tighter size control and lower surface roughness than conventional rough machining alone Grinding burn, wheel loading, residual stress, smearing, and loss of edge definition may occur without suitable wheel selection and coolant management. Use an appropriate open-structure abrasive wheel, controlled infeed, effective coolant application, frequent dressing, and final dimensional verification. State Ra or other surface-finish requirements, flatness, roundness, waviness, edge-break limits, and whether non-destructive testing is required.
Electrical Discharge Machining
Intricate slots, narrow openings, hard-to-reach profiles, and difficult geometries
Grade 5
Often considered for complex conductive titanium parts

Grade 23
May be used where the component specification permits EDM
Fine slots, intricate profiles, small apertures, and features that are difficult to produce with conventional cutting tools Titanium is electrically conductive, allowing EDM processes. The final condition may include a recast layer and heat-affected material that must be evaluated for the application. Minimizes mechanical cutting forces and can produce complex features in hardened or difficult-to-access areas Slower material removal, electrode wear, recast-layer formation, and possible changes to surface integrity require process and post-process control. Define acceptable surface integrity, use finishing passes, clean the workpiece thoroughly, and inspect critical surfaces when required by the end-use specification. Clarify whether EDM is permitted, specify recast-layer limits, dimensional tolerances, surface-finish requirements, and post-EDM cleaning or polishing.
Material classification note: ASTM Grade 2 is commercially pure titanium, while ASTM Grade 5 is Ti-6Al-4V. ASTM Grade 23 is Ti-6Al-4V ELI, an extra-low-interstitial variant. Actual mechanical properties and machinability depend on product form, heat treatment, material condition, tooling, machine rigidity, and the applicable ASTM or customer specification.

Choose the Process: CNC Milling, Turning, Drilling, EDM, or Grinding

In 2026, global buyers are choosing titanium machining processes based on geometry, tolerance, volume, and surface requirements. Titanium resists corrosion, yet it also traps heat near the cutting edge. That heat can damage tools quickly. Experienced machinists therefore use sharp carbide tooling, controlled feeds, and steady coolant delivery.

CNC milling suits complex housings, pockets, and contoured aerospace-style components. It provides flexible tool paths and accurate feature positioning. Turning is more efficient for shafts, rings, and symmetrical parts. Drilling needs special attention because deep holes may collect chips and increase heat. Short peck cycles help, but they can reduce productivity. EDM handles difficult profiles and hardened sections without applying heavy cutting force. Its slower removal rate may disappoint buyers with large production volumes. Grinding creates precise finishes on critical surfaces, although excessive pressure can cause burning or unwanted distortion.

The best choice depends on the drawing, not the material name alone. A hybrid route may work better: turning for the basic form, milling for features, and grinding for final tolerance. I still question overly tight tolerances when the assembly does not need them. They increase cost and inspection time. Small details matter. Buyers should confirm hole depth, corner radius, finish requirements, batch size, and inspection methods before production. A process trial using the actual titanium grade can reveal chatter, burrs, or heat problems early. That practical evidence is often more reliable than a standard process chart.

Control Heat and Wear: ISO 513 Tools, Low Speeds, and Chip Evacuation

2026 Top Titanium Machining Types for Global Buyers

Control Heat and Wear: ISO 513 Tools, Low Speeds, and Chip Evacuation

Titanium machining punishes careless settings. Its low thermal conductivity traps heat near the cutting edge. A practical starting point uses ISO 513 S-group tool materials for heat-resistant alloys. However, ISO 513 is not a complete process recipe. Tool geometry, workpiece grade, and machine rigidity still matter.

Keep cutting speeds conservative, then adjust feed carefully. Excessive speed can create a bright, overheated edge within minutes. Too little feed may cause rubbing instead of cutting. That mistake is easy to miss. I have seen operators blame the tool when the real problem was a weak chip load. Sharp edges, positive geometry, and adequate clearance usually reduce friction. Coated carbide may work well, but tool life must be verified through controlled trials.

Chip evacuation deserves equal attention. Use generous flute space and direct coolant toward the cutting zone. Long, stringy chips can wrap around the tool or scratch a finished surface. Through-tool coolant helps in deep pockets, although access can remain uneven. Reduce radial engagement when possible, and avoid sudden tool stops inside the material. Inspect the edge after each trial, not only after failure. Results vary across machines, and published cutting data should be treated as a starting point, not a guarantee.

Qualify Global Suppliers: ASTM B348, ASME B46.1, and ISO 9001 Records

2026 Top Titanium Machining Types for Global Buyers

Qualifying a titanium supplier starts with records, not polished photographs. ASTM B348 verifies requirements for titanium and titanium alloy bars and billets, including chemistry, mechanical properties, and dimensional controls. Ask for the exact heat number, mill test report, and matching inspection results. A missing link between these documents creates risk.

ASME B46.1 helps buyers evaluate surface texture after turning, milling, or grinding. Request Ra values, measurement direction, instrument calibration dates, and sampling locations. A reported Ra value without measurement conditions is weak evidence. ISO’s Survey of Management System Standard Certifications 2023 shows ISO 9001 remains the most widely adopted quality standard across more than 180 economies. Yet certification alone does not prove machining capability. Review internal audit findings, nonconformance records, corrective actions, and calibration logs. In practice, clean paperwork can still hide unstable tool wear. That point deserves more attention.

Tips: Compare three recent production records, not one perfect sample. Confirm that ASTM B348 material certificates match the finished part. Check whether ASME B46.1 readings come from the critical sealing or contact surfaces. Ask for supplier-controlled revisions and employee training records. USGS Mineral Commodity Summaries 2024 continues to identify titanium as an important strategic material, but availability does not replace process discipline. I would also request a small trial order. It costs more upfront, but it exposes weak traceability early.

2026 Top Titanium Machining Types for Global Buyers

Material strength profile for titanium grades commonly selected for turning, milling, drilling, and grinding applications.

Buyer qualification guidance: ASTM B348 records should confirm the titanium grade, product form, heat treatment, chemical composition, and mechanical properties. ASME B46.1 should be used to verify surface texture requirements for machined parts. ISO 9001 records provide evidence of a documented quality management system, but they should be reviewed together with material certificates, inspection reports, and process-control records.

Strength values shown are minimum specified values in MPa for commonly referenced ASTM B348 titanium bar grades. Requirements may vary by grade, product condition, and applicable specification revision.

FAQS

How should buyers choose a titanium machining process?

Base the choice on geometry, tolerance, production volume, and surface requirements. Material type alone is not enough. Review the drawing carefully.

When is CNC milling suitable for titanium parts?

CNC milling suits complex housings, pockets, and contoured components. It supports flexible tool paths and accurate feature positioning. Sharp carbide tools help control heat.

When should turning be used instead?

Turning works well for shafts, rings, and symmetrical parts. It usually removes material efficiently from round forms. The process may not suit irregular features.

What problems can occur during titanium drilling?

Deep holes can trap chips and increase heat. Short peck cycles improve chip removal. However, they may reduce production speed. Hole depth deserves close review.

When is EDM a practical option?

EDM suits difficult profiles and hardened sections. It applies less heavy cutting force than conventional cutting. Its slower removal rate may disappoint during large production runs.

Why is grinding used for titanium parts?

Grinding creates precise finishes on critical surfaces. Excessive pressure can cause burning or distortion. Steady control matters more than aggressive material removal.

Can several machining processes be combined?

Yes. A mixed route may improve results. Turning can create the basic form, milling can add features, and grinding can finish tight surfaces. This route may increase handling time.

What supplier records should buyers request?

Request material certificates, heat numbers, test reports, inspection results, and controlled drawing revisions. Match the material records with the finished part. Missing links create risk.

How should surface finish claims be checked?

Ask for Ra values, measurement direction, instrument calibration dates, and sampling locations. Check critical sealing or contact surfaces. A number without conditions proves little.

Does quality certification prove machining capability?

No. Certification shows a management framework, not stable tool performance. Review audits, corrective actions, calibration logs, and nonconformance records. Clean paperwork can still hide tool wear. That risk is easy to underestimate.

Conclusion

Titanium Machining in 2026 requires a clear understanding of titanium’s physical properties, including its approximate density of 4.5 g/cm³ and melting point of 1,668°C. Global buyers should first identify the appropriate ASTM grade for their application, such as Grade 2 for general corrosion resistance, Grade 5 Ti-6Al-4V for high strength, or Grade 23 for enhanced ductility and medical-related performance. The selected grade directly influences cutting parameters, tooling, and quality requirements.

Common processes include CNC milling, turning, drilling, electrical discharge machining, and grinding. Because titanium generates heat and can accelerate tool wear, manufacturers should use suitable ISO 513 tool materials, conservative cutting speeds, stable fixturing, effective cooling, and reliable chip evacuation. When evaluating international suppliers, buyers should review ASTM B348 material records, ASME B46.1 surface-finish results, and ISO 9001 quality-management documentation. These checks help confirm consistent material properties, dimensional accuracy, surface quality, and dependable production control.
Liam

Liam

Liam is a dedicated marketing professional with a profound expertise in the industry, where he excels at highlighting the unique advantages of our core products. With a keen understanding of market trends and consumer needs, Liam frequently updates our company’s professional blog, providing......